
Aerospace Manufacturing
Powder, coating, composite
and resin behavior across aerospace manufacturing
Alloy powders, ceramics, coating feedstocks, reinforcements, polymers and resin systems are not one category
Oxygen, moisture, particle size, morphology, satellites, density, purity, electrostatics, rheology and thermal history decide whether a feedstock spreads, feeds, deposits, wets out, bonds, cures and qualifies. Reuse history compounds all of it. This page connects what you are seeing on the line to the mechanism behind it and the measurement that settles it.


Find your route
Start with the material, then the behavior
Aerospace materials do not behave as one category. Pick the alloy powder, ceramic, coating feedstock, reinforcement, polymer, adhesive, microsphere, sealant or reclaimed material class, then the behavior you are seeing in the process. The result names the mechanisms worth separating, the measurement to start with, and where in the process it usually shows up. It is a triage route, not a diagnosis.
- 1Material
- 2Behavior
- 3Route
Step 1 What are you handling?
Step 2 What are you seeing?
Step 3 Your route
Material routes
Alloy powders, ceramics, coatings, composites and resin systems
Aerospace manufacturing handles reactive metal powders, dense superalloys, high-temperature ceramics, classified coating feedstocks, fibrous reinforcements, high-performance polymers, filled resins, lightweight microspheres, sealants and reclaimed process streams with very different sensitivities to oxygen, moisture, particle size, morphology, density, electrostatics, thermal history, shear, contamination and reuse. Each class has its own behavior profile, so the most useful route starts with the material before moving to the visible defect or process instability.
Aluminum alloy powders and fines
Aluminum powders and machining fines require controlled oxidation, particle size, and contamination. Morphology, fines, storage, and reuse influence spreading, feeding, and part quality.
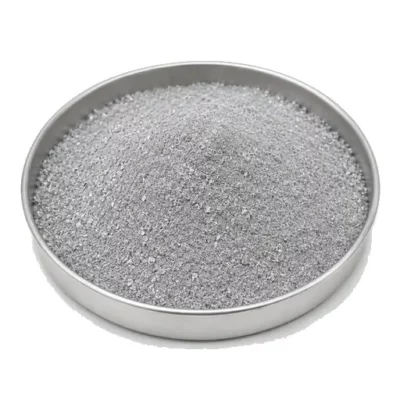
Titanium and titanium alloy powders
Titanium powders are sensitive to oxygen pickup and handling history. Particle shape, satellites, fines, moisture, and reuse affect flow, layer formation, and mechanical performance.
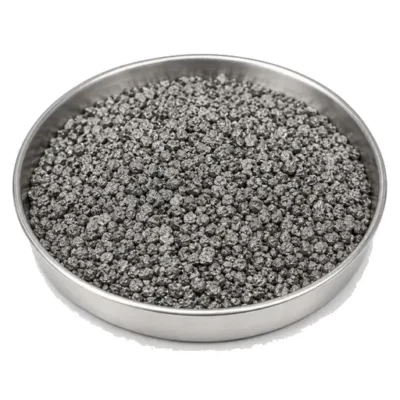
Nickel-based superalloy powders
Nickel superalloy powders require stable chemistry and morphology. Size distribution, satellites, oxidation, contamination, and reuse influence feeding, melting, and high-temperature properties.
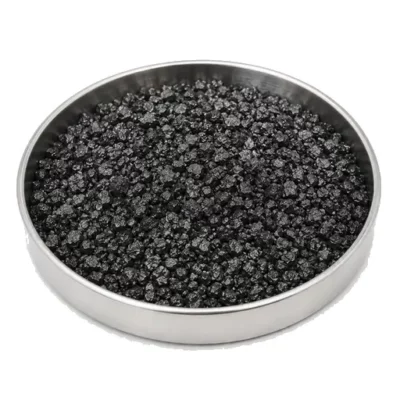
Cobalt and refractory alloy powders
Cobalt, tungsten, and refractory alloy powders combine high density with demanding purity controls. Segregation, oxidation, morphology, and feeding affect deposition and performance.
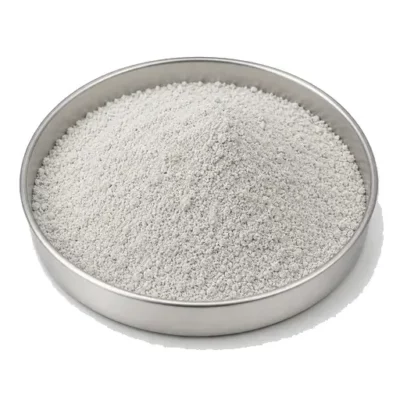
High-temperature ceramic powders
Ceramic powders for thermal, insulating, and wear-resistant parts require controlled agglomeration and purity. Moisture, particle size, chemistry, and sintering affect final density.
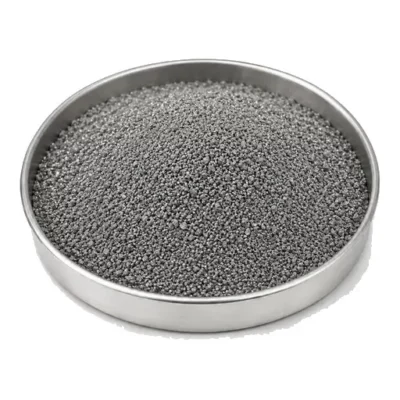
Thermal-spray coating powders
Thermal-spray powders require controlled feedstock size and morphology. Oversize particles, fines, hollow particles, oxidation, and feeder variation affect deposition and coating structure.
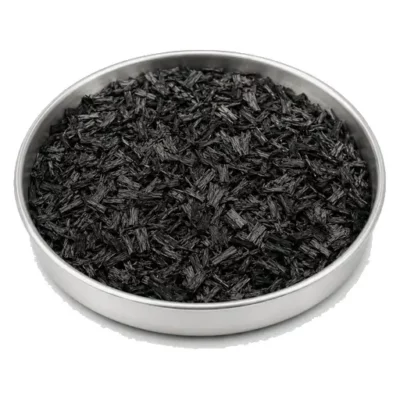
Composite reinforcement materials
Chopped carbon fibers and particulate reinforcements require controlled length and distribution. Breakage, electrostatics, segregation, orientation, and wetting affect strength.
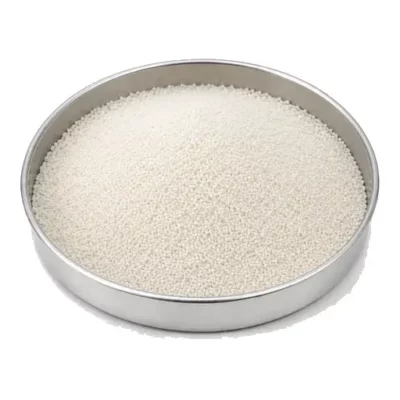
High-performance polymer powders
PEEK, PEKK, and related polymer powders require controlled moisture and thermal history. Particle size, flow, aging, and incomplete fusion affect stability and component properties.
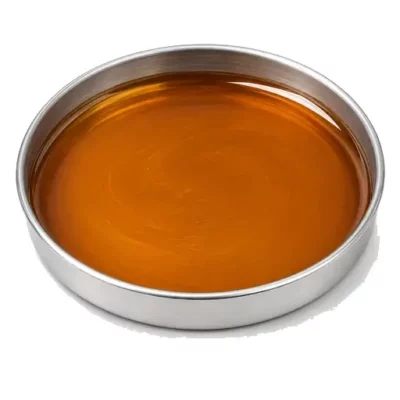
Structural adhesives and resin systems
Structural adhesives and resin systems require controlled viscosity, wetting, and cure response. Filler settling, moisture, air entrainment, aging, and temperature affect reliability.
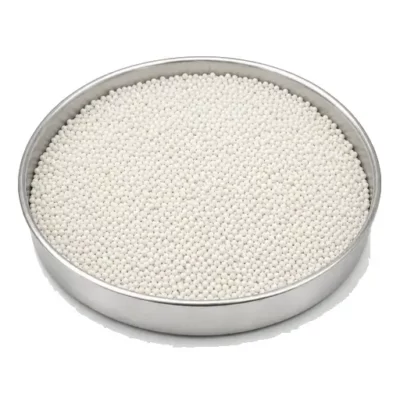
Lightweight fillers and microspheres
Hollow microspheres and lightweight fillers reduce density but can break or segregate. Particle strength, size distribution, mixing intensity, and wetting influence performance.
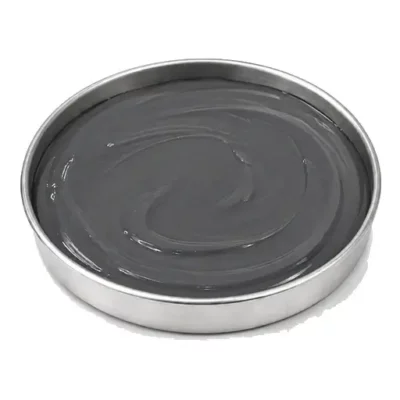
Sealants and potting compounds
Sealants and potting compounds require stable rheology and filler distribution. Settling, moisture, air entrapment, cure variation, and dispensing history affect long-term reliability.
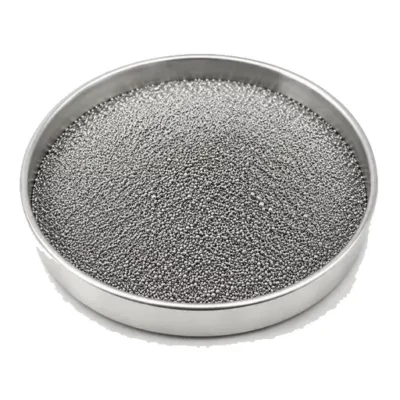
Reclaimed manufacturing streams
Reclaimed powders, machining fines, and coating residues have mixed composition and history. Contamination, oxidation, size, liberation, and reuse limits determine recovery consistency.
Quick comparison
Material route, common risk, first measurement
The same symptom points to different mechanisms depending on the material class, particle morphology, atmosphere, surface condition, formulation, handling history and process step. This is the fast bridge between aerospace material behavior and the most useful first measurement route.
Aerospace material routes, the handling or processing risk each one carries most often, and the measurement worth running first.
| Material route | Common handling or processing risk | Useful first measurement |
|---|---|---|
| Aluminum alloy powders and fines | Oxidation, fines accumulation, contamination, poor spreading, and inconsistent consolidation | Particle size, morphology, oxygen, flowability, and contamination |
| Titanium and titanium alloy powders | Oxygen pickup, satellites, unstable flow, poor layers, and reuse-related variation | Oxygen, particle size, morphology, flowability, and reuse history |
| Nickel-based superalloy powders | Chemistry drift, satellites, oxidation, poor feeding, and melt pool instability | Composition, particle size, morphology, oxygen, and flowability |
| Cobalt and refractory alloy powders | Segregation, oxidation, density-driven feeding variation, and inconsistent deposition | Composition, density, particle size, morphology, and oxygen |
| High-temperature ceramic powders | Agglomeration, moisture uptake, contamination, poor shaping, and density variation | Particle size, moisture, surface chemistry, purity, and sintering response |
| Thermal-spray coating powders | Fines, oversize particles, hollow particles, feeder variation, and coating defects | Particle size, morphology, density, flowability, and feed response |
| Composite reinforcement materials | Fiber breakage, electrostatics, segregation, poor orientation, and weak wetting | Fiber length, morphology, dispersion, electrostatics, and wetting |
| High-performance polymer powders | Moisture, thermal aging, poor flow, incomplete fusion, and property variation | Moisture, particle size, flowability, thermal behavior, and melt response |
| Structural adhesives and resin systems | Viscosity drift, poor wetting, filler settling, air entrainment, and cure variation | Rheology, wetting, filler distribution, moisture, and cure response |
| Lightweight fillers and microspheres | Breakage, segregation, dusting, poor dispersion, and density variation | Particle size, particle strength, density, morphology, and dispersion |
| Sealants and potting compounds | Settling, air entrainment, unstable dispensing, incomplete cure, and sealing defects | Rheology, filler distribution, air content, moisture, and cure response |
| Reclaimed manufacturing streams | Mixed composition, contamination, oxidation, poor liberation, and variable reuse quality | Composition, particle size, liberation, oxygen, and contamination screening |
One risk per row is the one most often reported, not the only one that occurs. Use the selector above to work a specific combination through to a route.
Recurring problems
Start from the behavior you can see
These eight come from your own route card and continue block: flow, caking, dust, dosing variation, segregation, contamination, oxidation and bonding or cure instability. Oxidation leads its own card here rather than sitting second behind moisture, because on this hub it is the behavior the copy leans on hardest. Each card runs back to the mechanisms worth separating and forward to the measurement that confirms which one is governing.




Also covered: agglomeration, attrition, electrostatics, spreading & deposition. All symptoms
Measurement routes
The test that answers your question
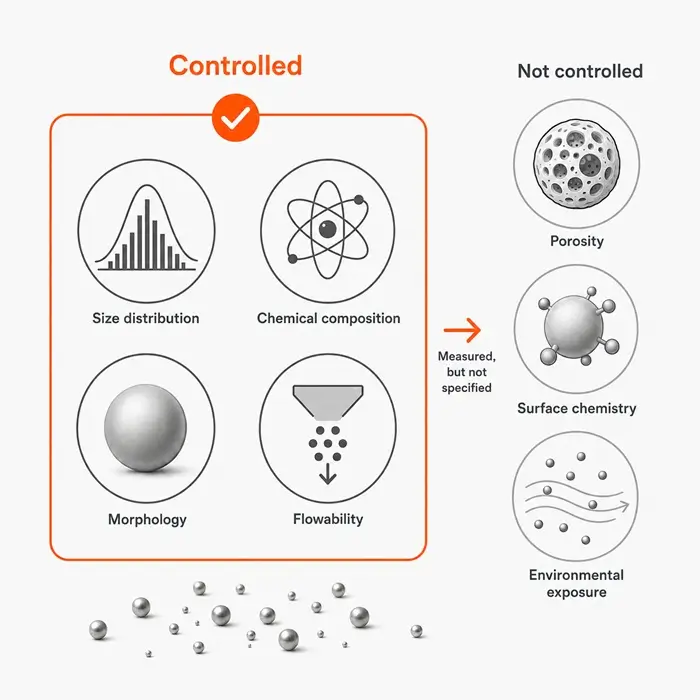
Aerospace material behavior rarely resolves to one number. Particle size, morphology, oxygen, moisture, alloy chemistry, surface condition, cohesion, density, electrostatics, fiber dimensions, rheology, wetting, thermal response, contamination and reuse history can all sit behind the same visible process symptom or component defect. Pick the method by the question, not by the symptom.
Compare every method All test methods on the site, grouped by the question they answer.
Process routes
Where the behavior actually shows up
The same aerospace material behaves differently depending on where it sits in the process. Powder production, storage and atmosphere control, additive manufacturing, thermal spraying, composite processing, bonding, curing, thermal processing, finishing and recovery each expose a different property, a different contamination pathway and a different failure mode.
Go deeper
Guides and articles for aerospace materials
Longer reads that work through the mechanisms behind these routes, from the visible process problem to material properties, measurement choice and qualification.

FAQ
Aerospace material questions
Need the measurement, not just the guidance? PowderTechnology.info works closely with Delft Solids Solutions,
a contract research organization specializing in the physical behavior of powders and granules. DSS provides
contract testing and characterization, with its laboratory working in accordance with ISO 17025.
Contact Delft Solids Solutions.