SUBJECT
Flowability
Publications on powder flow, flowability testing, cohesive behavior, and the material and process factors that influence reliable handling and discharge.
PUBLICATIONS
Browse publications
Explore PTI articles, Insights, Know How, and technical publications related to this subject.
 24 October 2026
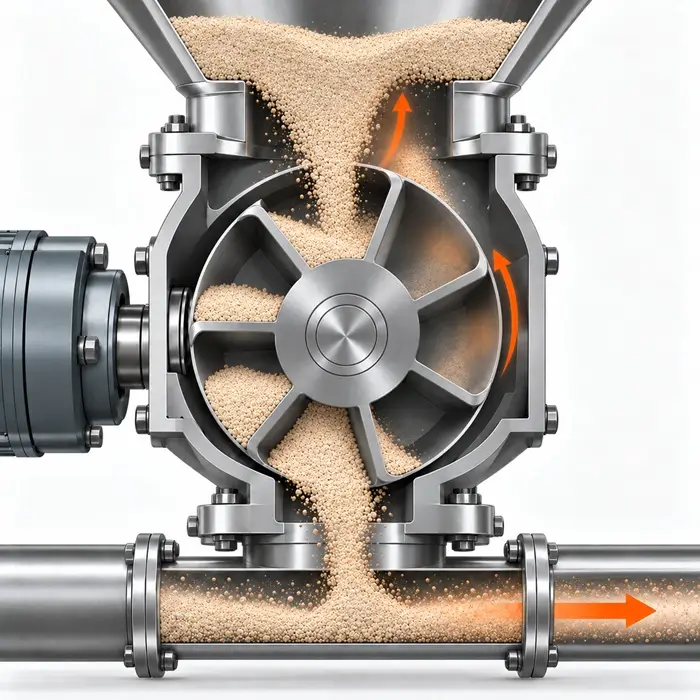
Rotary Valve Failure Modes: How Powder Properties Drive Leakage, Wear, and Jamming
When a rotary airlock valve leaks, wears, or jams, the cause usually lies in the powder rather than the equipment. This insight maps cohesion, abrasiveness, bulk density, and particle size distribution to distinct failure patterns and explains what each pattern tells you about the powder state.
Insights
 20 October 2026
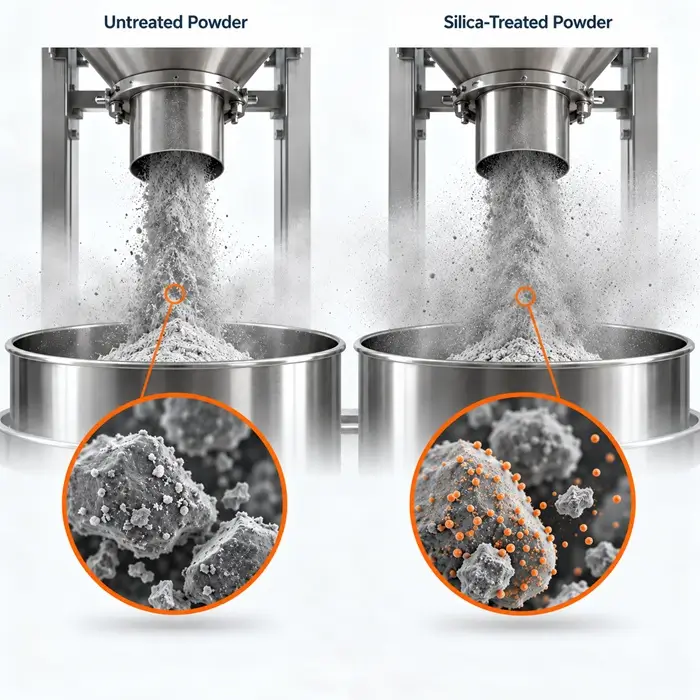
Why Can Anti-Caking Agents Increase Dustiness?
An additive that improves powder flow or caking resistance can also increase [...]
 19 October 2026
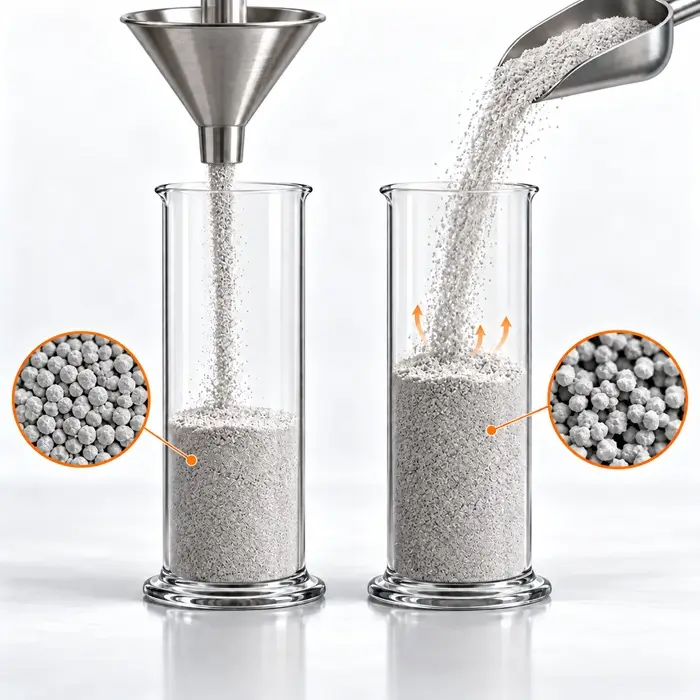
Why Does Pouring Method Change Bulk Density?
Loose bulk density depends on how powder enters the measuring container. Funnel [...]
 17 October 2026
LFP Cathode Powder Production: How Spray-Drying, Calcination, and Pulverization Set Particle Size and Tap Density Targets
LFP cathode powder quality is built in stages, not inspected at the end. This article follows the precursor-to-powder route and shows why particle size distribution and tap density are the measurements that actually tell you whether the synthesis worked.
Feature Article
 14 October 2026
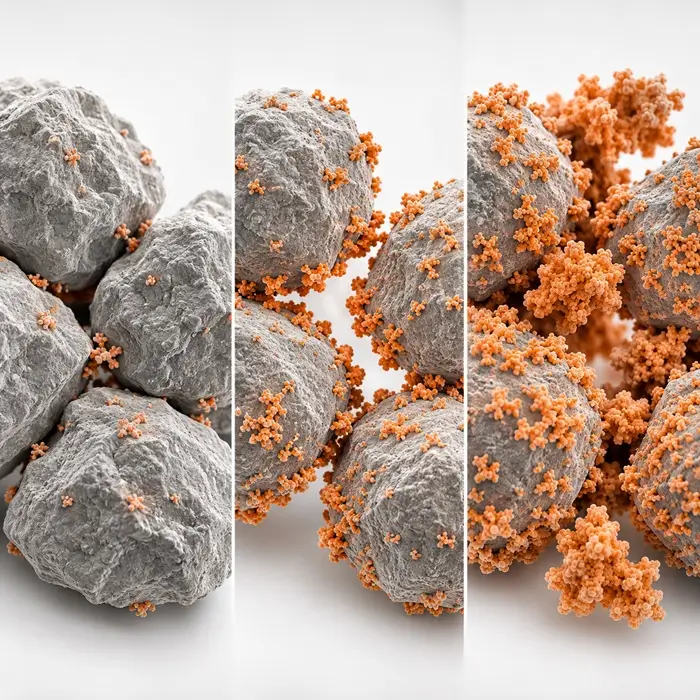
Why Does Too Much Silica Make Powder Flow Worse?
Fumed (colloidal) silica improves powder flow by separating host particles and reducing [...]
 13 October 2026
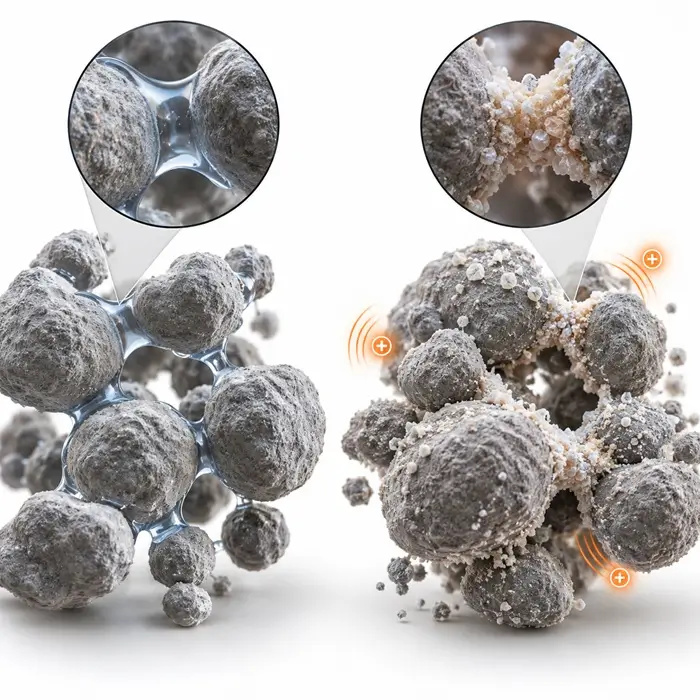
Why Does Powder Become More Cohesive After Drying?
Drying does not always improve powder flow. Dissolved material can form solid [...]
 10 October 2026
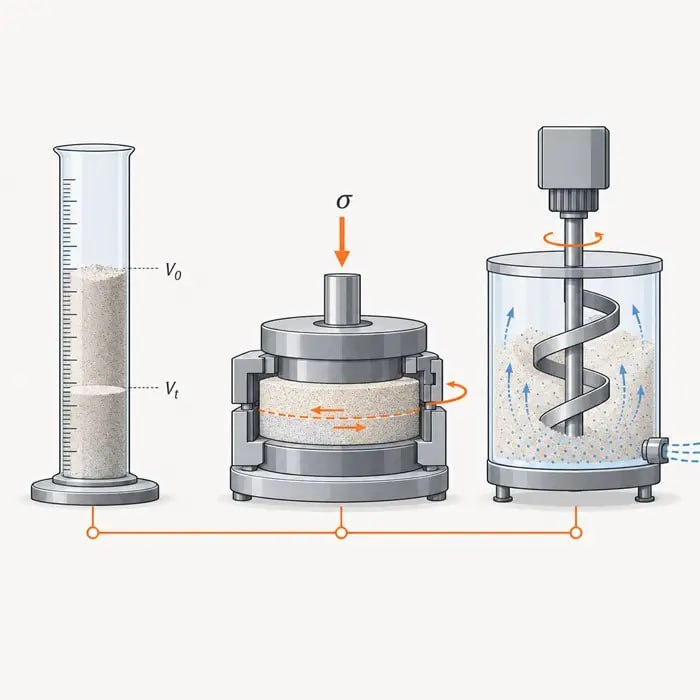
PBF Powder Flowability Testing: Why Different Methods Disagree and What the Results Mean
Hausner ratio, shear cell, and dynamic flow energy results on the same PBF powder lot rarely agree exactly. That disagreement is a decision input, not proof that a method or lab got it wrong.
Insights
 3 October 2026
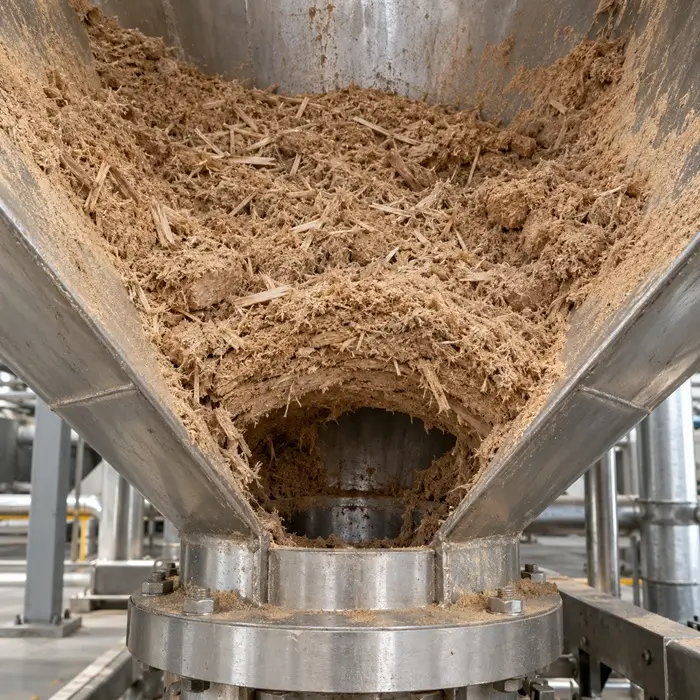
Wood Powder Feeding Problems: Separating Moisture Effects From Particle Interlocking
Wood powder can bridge because fibrous particles mechanically interlock, because moisture increases [...]
Feature Article
 3 October 2026
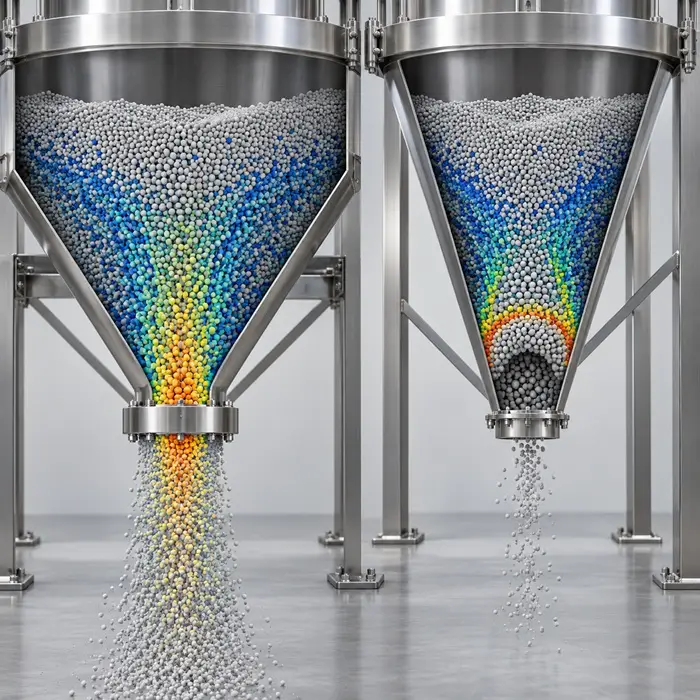
DEM Calibration: Why a Model That Reproduces One Bulk Test Can Still Fail in a Different Hopper Geometry
DEM input parameters are fitted to match a bulk observable, not derived from first principles. A parameter set calibrated against an angle of repose test constrains one point in a multi-dimensional parameter space. When the hopper geometry changes, the stress state changes, and unconstrained parameters become the dominant source of prediction error.
Insights
 26 September 2026
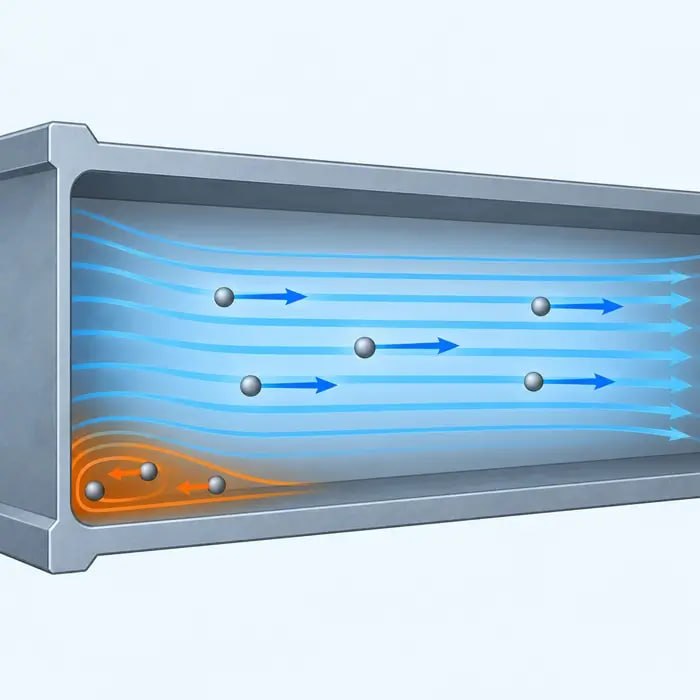
Triboelectric Particle Back-Flow in Pneumatic Conveying: Why Charged Particles Migrate Upstream at Duct Corners
CFD-DEM simulations show triboelectrically charged particles can reverse direction in low-drag duct corner zones during pneumatic conveying, with the delay between feed pulses driving the effect more than pulse length.
Insights
 19 September 2026
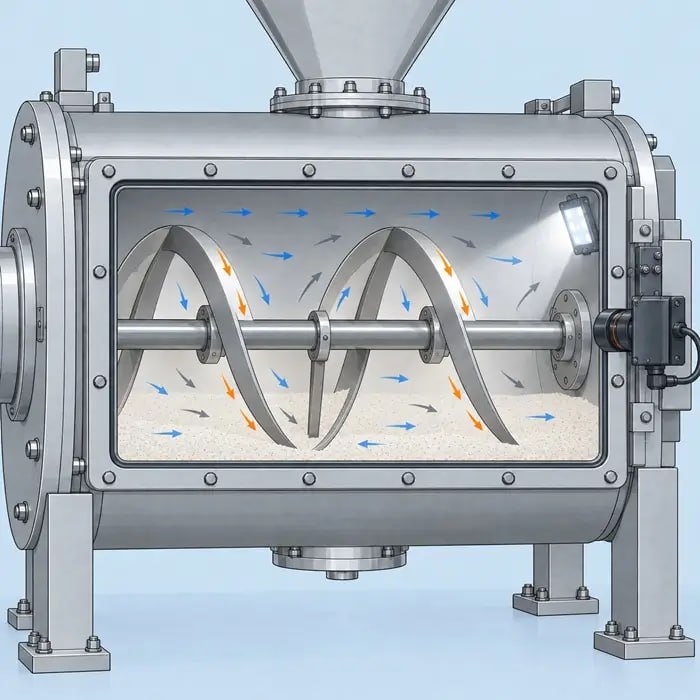
Real-Time Powder Flow Imaging: What LED-Based Particle Image Velocimetry Adds Beyond Static Flowability Tests
LED-based particle image velocimetry (PIV) images the velocity field inside a moving powder bed during blending, adding spatial resolution that static angle of repose, Hausner ratio, and shear cell tests cannot provide. Here is what that resolution can and cannot support for a process decision.
Insights
 12 September 2026
Powder-Fed Laser Cladding: Why Stable Feed Rate Does Not Guarantee Stable Deposition
In powder-fed laser cladding, a stable feeder setpoint and an in-spec particle size distribution do not guarantee a stable deposit. Catchment efficiency and stream divergence sit between the feeder and the melt pool, and both can drift independently of the powder's PSD.
Insights