Battery materials
Active material, precursor, conductive additive and recycled powder behavior in battery production
Salts, precursors, active materials, additives and black mass are not one category
Particle size, shape, moisture, cohesion, bulk density, surface condition, agglomeration and electrostatic behavior decide whether a battery material flows, doses evenly, disperses, coats uniformly, and holds its electrochemical performance. This page connects what you are seeing on the line to the mechanism behind it and the measurement that settles it.
Battery materials
Active material, precursor, conductive additive and recycled powder behavior
in battery production
Salts, precursors, active materials, additives and black mass are not one category
Particle size, shape, moisture, cohesion, bulk density, surface condition, agglomeration and electrostatic behavior decide whether a battery material flows, doses evenly, disperses, coats uniformly, and holds its electrochemical performance. This page connects what you are seeing on the line to the mechanism behind it and the measurement that settles it.


Find your route
Start with the material, then the behavior
Battery materials do not behave as one category. Pick the precursor, active material, anode, additive, coating, electrolyte or recycled material class, then the behavior you are seeing in the process. The result names the mechanisms worth separating, the measurement to start with, and where in the process it usually shows up. It is a triage route, not a diagnosis.
- 1Material
- 2Behavior
- 3Route
Step 1 What are you handling?
Step 2 What are you seeing?
Step 3 Your route
Material routes
Precursors, active materials, additives and recovered streams
Battery material production handles fine powders, coated particles, conductive additives, salts, agglomerates, slurries and recovered streams with very different particle sizes, densities, surface chemistries, moisture sensitivities and electrostatic behaviors. The same site may handle lithium salts, hydroxide precursors, layered oxides, phosphate cathodes, graphite, silicon composites, conductive carbons, binders, ceramic powders, electrolyte materials and black mass. Each class has its own behavior profile, so the most useful route starts with the material.
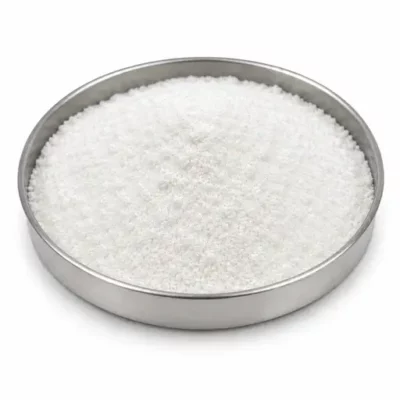
Lithium carbonate and hydroxide salts
Lithium carbonate and hydroxide powders can absorb moisture, cake, and segregate during storage. Particle size, purity, and handling history influence flow, dosing, dissolution, and reaction consistency.
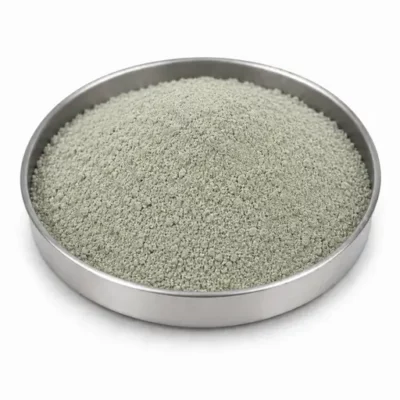
Nickel, cobalt, manganese precursors
Nickel, cobalt, and manganese precursor powders are fine, dense, and highly surface-sensitive. Moisture, agglomeration, and composition variation affect feeding, mixing, calcination, and final stoichiometry.
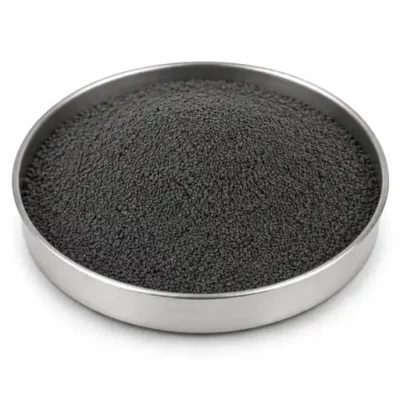
NMC and NCA cathode active materials
NMC and NCA powders require controlled particle size, morphology, residual lithium, and surface condition. Agglomeration, moisture, and breakage affect flow, slurry preparation, coating, and cell performance.
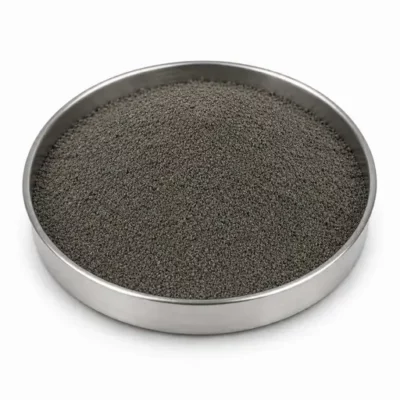
LFP and LMFP cathode active materials
LFP and LMFP powders vary in carbon coating, particle size, porosity, and agglomeration. These properties directly influence powder flow, dispersion, electrode density, electrical conductivity, and rate performance.
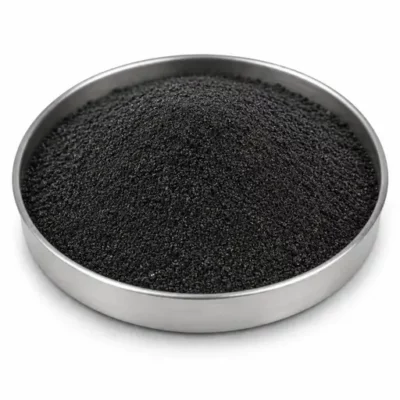
Natural and synthetic graphite anode materials
Natural and synthetic graphite powders differ in shape, tap density, surface area, and orientation. These differences affect flow, slurry rheology, coating, calendering, and electrode density.

Silicon and silicon-carbon anode materials
Silicon and silicon-carbon powders can be cohesive, reactive, and highly surface-sensitive. Particle size, oxidation, agglomeration, and blending influence dispersion, expansion, and cycle life.
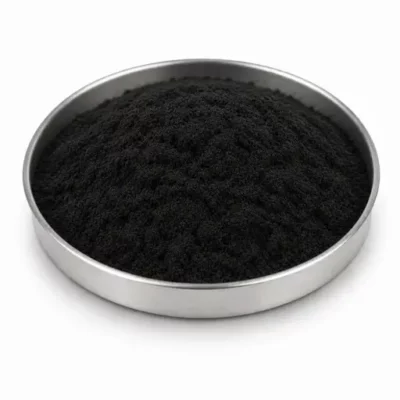
Conductive carbon and nanotube additives
Carbon black, graphite additives, and nanotubes are low-density, dusty, and strongly cohesive. Surface area, structure, and dispersion determine feeding, conductivity, and coating uniformity.
Binder powders and rheology control additives
PVDF, CMC, and related binder powders can agglomerate, charge, and absorb moisture. Particle size, addition sequence, and dissolution behavior directly influence slurry stability and adhesion.
Ceramic separator and coating powder materials
Alumina, boehmite, and other ceramic powders require controlled size, purity, and dispersion. Agglomeration, abrasiveness, and settling affect coating stability, separator uniformity, and overall safety.
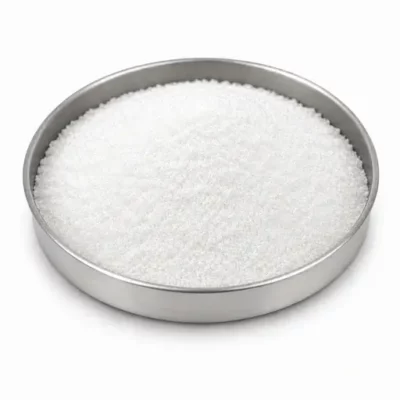
Electrolyte salts and solid electrolyte powders
Electrolyte salts and solid electrolyte powders are highly sensitive to moisture, contamination, and surface change. Handling conditions influence flow, ionic conductivity, processing, and safety.
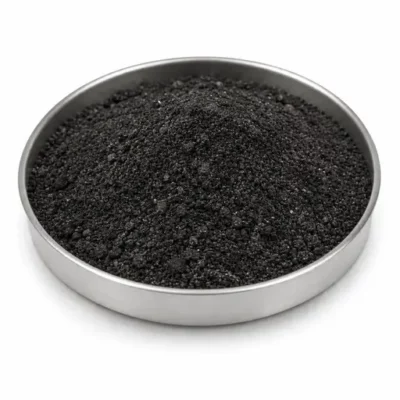
Recycled black mass and recovered powders
Recycled black mass combines cathode, anode, carbon, metal, and binder residues. Composition, moisture, particle size, and contamination directly affect storage, separation, refining, and recovery.
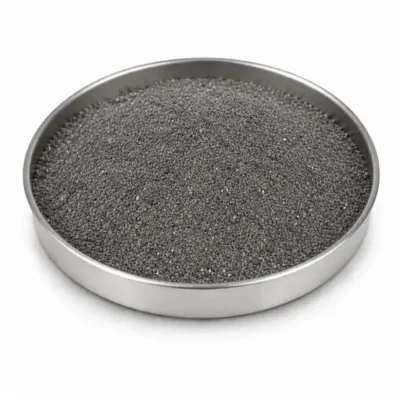
Dry electrode and premixed powder blends
Dry electrode and premixed powder blends combine active material, conductive additive, and binder. Density contrast, electrostatics, and mixing history directly influence final blend uniformity and consistent feeding.
Quick comparison
Material route, common risk, first measurement
The same symptom points to different mechanisms depending on the material class, surface condition, moisture state and process step. This is the fast bridge between battery material behavior and the most useful first measurement route.
Battery material routes, the handling or processing risk each one carries most often, and the measurement worth running first.
| Material route | Common handling or processing risk | Useful first measurement |
|---|---|---|
| Lithium carbonate and hydroxide salts | Moisture uptake, caking, agglomeration, and dosing variation | Moisture, particle size, bulk density, and flowability |
| Nickel, cobalt, and manganese precursors | Morphology variation, agglomeration, moisture, and unstable calcination feed | Particle size, morphology, moisture, and tap density |
| NMC and NCA cathode active materials | Segregation, dustiness, agglomeration, and coating variation | Particle size, morphology, surface area, and moisture |
| LFP and LMFP cathode active materials | Carbon coating variation, cohesion, agglomeration, and compaction differences | Particle size, tap density, moisture, and surface characterization |
| Natural and synthetic graphite anodes | Segregation, dust release, poor wetting, and coating inconsistency | Particle shape, size distribution, surface area, and density |
| Silicon and silicon-carbon anode materials | Agglomeration, oxidation, density contrast, and blend instability | Particle size, surface condition, oxidation, and blend uniformity |
| Conductive carbon and nanotube additives | Extreme cohesion, dustiness, static charging, and poor dispersion | Bulk density, electrostatics, wetting, and dispersion assessment |
| Binder powders and rheology additives | Agglomeration, moisture uptake, charging, and dissolution variation | Particle size, moisture, dissolution behavior, and viscosity response |
| Ceramic separator and coating powders | Agglomeration, poor dispersion, coating defects, and settling | Particle size, surface area, moisture, and dispersion stability |
| Electrolyte salts and solid electrolyte powders | Moisture sensitivity, contamination, agglomeration, and conductivity loss | Moisture, purity, particle size, and surface condition |
| Recycled black mass and recovered powders | Variable composition, contamination, moisture, and separation difficulty | Composition, particle size, moisture, and contamination screening |
| Dry electrode and premixed powder blends | Segregation, electrostatic charging, density contrast, and feeding variation | Blend uniformity, bulk density, electrostatics, and flowability |
One risk per row is the one most often reported, not the only one that occurs. Use the selector above to work a specific combination through to a route.
Recurring problems
Start from the behavior you can see
These eight are the ones your own route card and continue block already name: flow, caking, dust, dosing, agglomeration, contamination, moisture and dispersion. Contamination earns a card here that it gets on no other hub, because a single metal particle can scrap a cell. Each card runs back to the mechanisms worth separating and forward to the measurement that confirms which one is governing.




Also covered: electrostatics, segregation, attrition, adhesion. All symptoms
Measurement routes
The test that answers your question
Battery material behavior rarely resolves to one number. Particle size, morphology, surface condition, moisture, cohesion, bulk density, electrostatic behavior, contamination and dispersion state can all sit behind the same visible process symptom. Pick the method by the question, not by the symptom.
Process routes
Where the behavior actually shows up
The same battery material behaves differently depending on where it sits in the process. Storage, milling, conveying, dosing, slurry preparation, coating, drying, cell filling and recycling each expose a different property and a different failure mode.
Go deeper
Guides and articles for battery material behavior
Longer reads that work through the mechanisms behind these routes, from the visible process problem to material properties, measurement choice and interpretation.

FAQ
Battery material processing questions
Need the measurement, not just the guidance? PowderTechnology.info works closely with Delft Solids Solutions,
a contract research organization specializing in the physical behavior of powders and granules. DSS provides
contract testing and characterization, with its laboratory working in accordance with ISO 17025.
Contact Delft Solids Solutions.