Chemical industry

Powder behavior in
chemical production

Salts, fines, catalysts and additives are not one category

Particle size, moisture sensitivity, cohesion, electrostatic behavior, bulk density, particle strength and surface chemistry decide whether a chemical powder flows, cakes, segregates, doses evenly, dusts, breaks, or disperses. This page connects what you are seeing on the line to the mechanism behind it and the measurement that settles it.
By material type icon

By material type

Salts, fine powders, catalysts, additives, surfactants, sensitive powders.

By observed behavior icon

By observed behavior

Flow, caking, dust, dosing, segregation, breakage, moisture, static.

By measurement route icon

By measurement route

The test that clearly separates one likely mechanism from another.

By process area icon

By process area

Storage, discharge, conveying, dosing, blending, milling, filling, and packaging.

Find your route

Start with the material, then the behavior

Chemical powders do not behave as one category. Pick the material type, then the behavior you are seeing in the process. The result names the mechanisms worth separating, the measurement to start with, and where in the process it usually shows up. It is a triage route, not a diagnosis.

  1. 1Material
  2. 2Behavior
  3. 3Route

Step 1  What are you handling?

Step 2  What are you seeing?

Step 3  Your route

Material routes

Chemical powder and bulk solid types

The same plant may handle crystalline salts, fine mineral intermediates, catalysts, carrier materials, polymer additives, surfactant powders, and sensitive materials. Each group carries its own behavior profile, so the most useful route starts with the material type.
Quick comparison

Material class, common risk, first measurement

The same symptom points to different mechanisms depending on the chemical powder type and the process step. This is the fast bridge between material behavior and measurement route.

Chemical powder and bulk solid classes, the risk each one carries most often, and the measurement worth running first.
Material typeCommon riskUseful first measurement route
Fine powders and mineral intermediatesDustiness and poor flowParticle size distribution, dustiness
Hygroscopic salts and crystalline solidsCaking and moisture responseMoisture content, sorption
Catalysts, carriers, and functional granulesAttrition and fines generationAttrition, particle size before and after
Polymer additives and compounding chemicalsFeeding and segregationBulk density, particle size
Surfactants and cleaning intermediatesCaking and dissolution behaviorMoisture, dissolution behavior
Reactive or sensitive powdersStatic and containmentElectrostatic behavior, dustiness

One risk per row is the one most often reported, not the only one that occurs. Use the selector above to work a specific combination through to a route.

Recurring problems

Start from the behavior you can see

These eight cover what actually gets reported in chemical plants. Each one runs back to the mechanisms worth separating and forward to the measurement that confirms which one is governing.

Icon representing poor flow and discharge

Poor flow or discharge

Arching · Bridging · Discharge

Icon representing caking or hardening

Caking or hardening

Moisture · Load · Storage

Icon representing dust formation

Dust formation

Fines · Handling · Containment

Icon representing dosing variation

Dosing variation

Density · Aeration · Feeding

Icon representing segregation

Segregation

PSD · Density · Uniformity

Icon representing particle breakage

Particle breakage

Attrition · Fines · Damage

Icon representing moisture sensitivity

Moisture sensitivity

Humidity · Stickiness · Stability

Icon representing electrostatic behavior

Electrostatic behavior

Charging · Adhesion · Buildup

Measurement routes

The test that answers your question

Chemical powder behavior rarely resolves to one number. Particle size, moisture, cohesion, wall friction, density, permeability, friability, electrostatic behavior and dustiness can all sit behind the same visible symptom. Pick the method by the question, not by the symptom.

Particle and morphology

Particle size distribution
Fines, segregation, dissolution, packing, dustiness, and product consistency.

Microscopy and morphology
Particle shape, surface condition, agglomeration, breakage, and dispersion.

Moisture and product stability

Moisture content and sorption behavior
Humidity response, caking, stickiness, storage stability, and drying history.

Water activity
Water availability, deliquescence, caking onset, and storage stability.

Flow and discharge

Flowability and shear testing
Cohesion, consolidation, hopper discharge, arching, ratholing, and storage load.

Wall friction testing
Hopper design, discharge limits, wall material choice, and sticking behavior.

Air, dust, and electrostatics

Dustiness testing
Airborne fines, containment, exposure risk, transfer, and packaging operations.

Electrostatic charge testing
Charging, adhesion, dust attraction, wall buildup, and handling instability.

Structure and handling damage

Permeability and deaeration
Air retention, bulk density change, unstable feeding, settling behavior, and refill effects.

Attrition and friability testing
Granule damage, fines generation, conveying stress, and repeated handling cycles.

Density and packing

Bulk and tapped density
Fill weight, aeration, compressibility, feeder behavior, and pack consistency.

Compare every method
All test methods on the site, grouped by the question they answer.

Process routes

Where the behavior actually shows up

The same chemical powder behaves differently depending on where it sits in the process. Each step exposes a different property and a different failure mode.

01

Storage and silos

Residence time, consolidation, moisture uptake and caking change bulk density and later discharge behavior.

02

Hoppers and discharge

Arching, ratholing, wall friction, aeration and permeability decide whether material leaves a vessel reliably.

03

Mechanical conveying

Shear, vibration, compaction and attrition alter particle condition and segregation risk during transport.

04

Pneumatic conveying

Air velocity, solids loading, particle size, density and attrition affect conveying stability and product condition.

05

Dosing and feeding

Bulk density variation, refill behavior, cohesion and segregation act directly on feed consistency.

06

Mixing and blending

Particle size, density, shape and cohesion drive blend development and the risk of segregation.

07

Milling and size reduction

Breakage changes particle size distribution, fines content, surface area and downstream behavior.

08

Packaging and filling

Air entrainment, settling, dustiness and bulk density affect fill weight, pack consistency and handling.

09

Dust collection and containment

Dustiness, particle size, electrostatic behavior and air handling govern capture efficiency and containment.

Go deeper

Guides and articles for chemical powder behavior

Longer reads that work through the mechanisms behind these routes, from the visible process problem to material properties, measurement choice and interpretation.
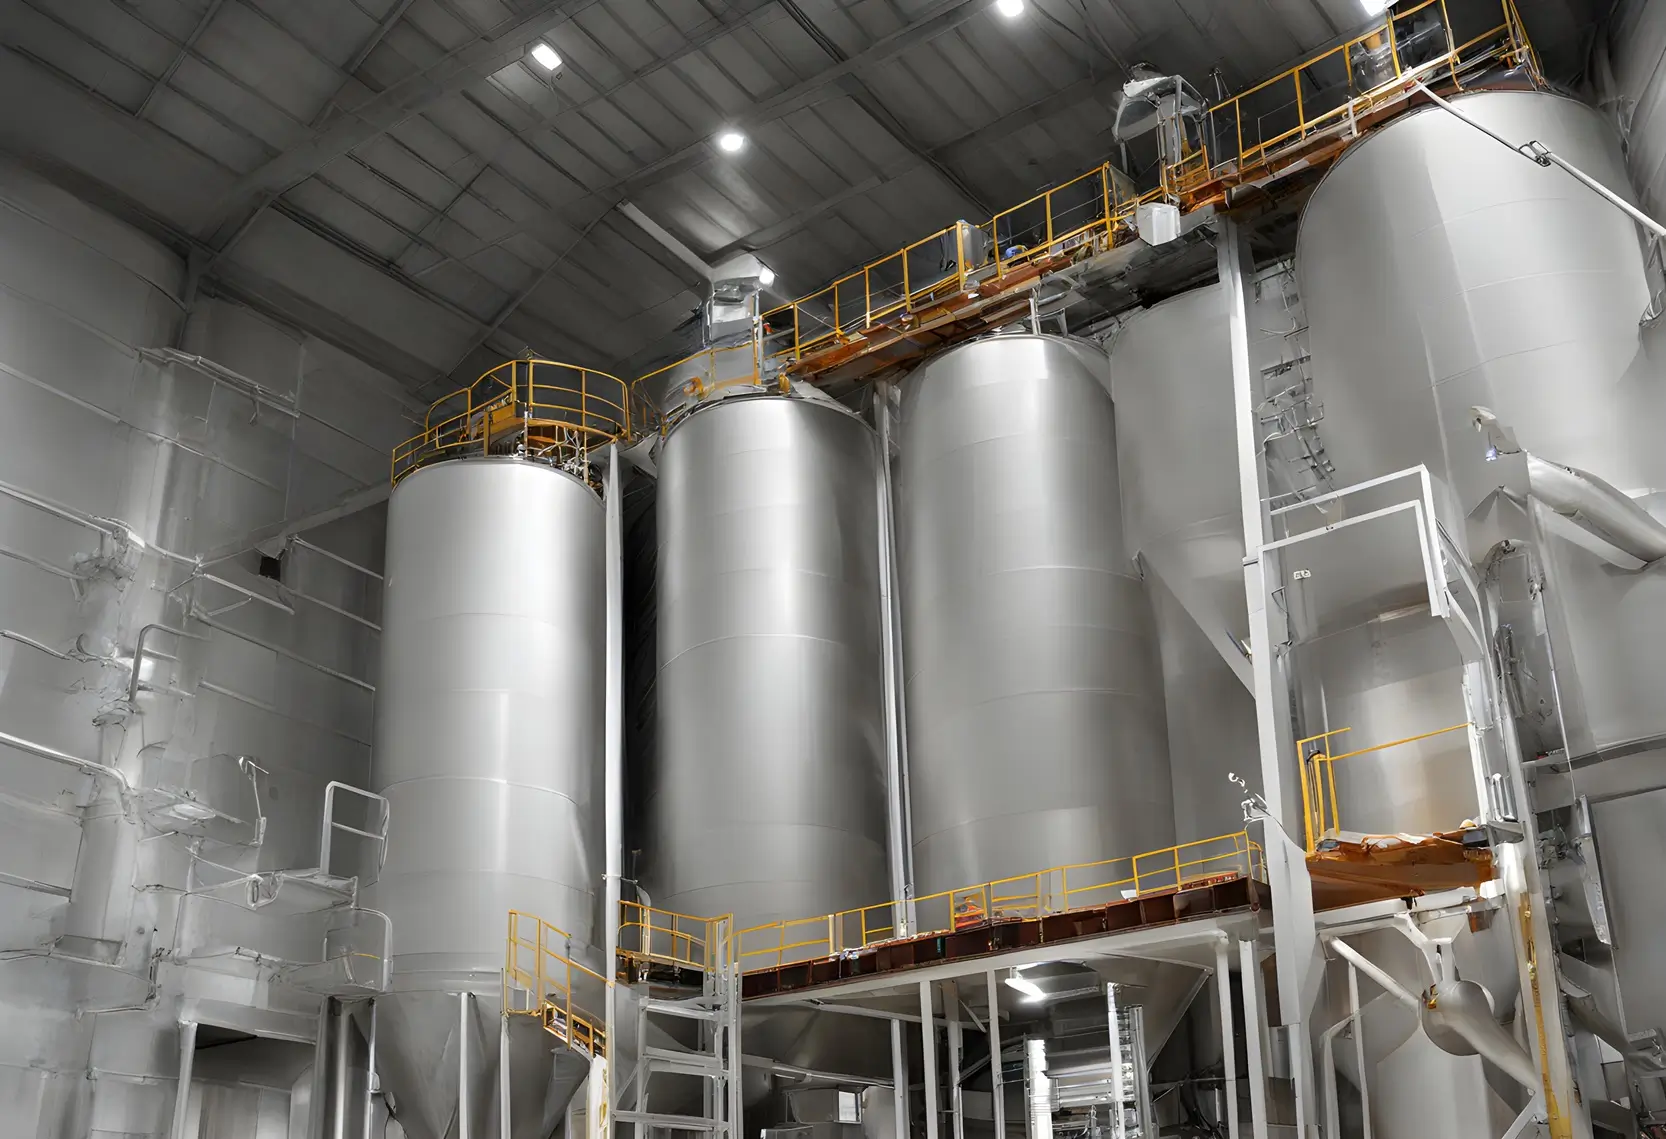
Industrial silo storage of bulk powder, with characterization data behind the design

Bulk powder characterization for silo storage

Which properties actually govern whether a silo discharges, and what to measure before the geometry is fixed.

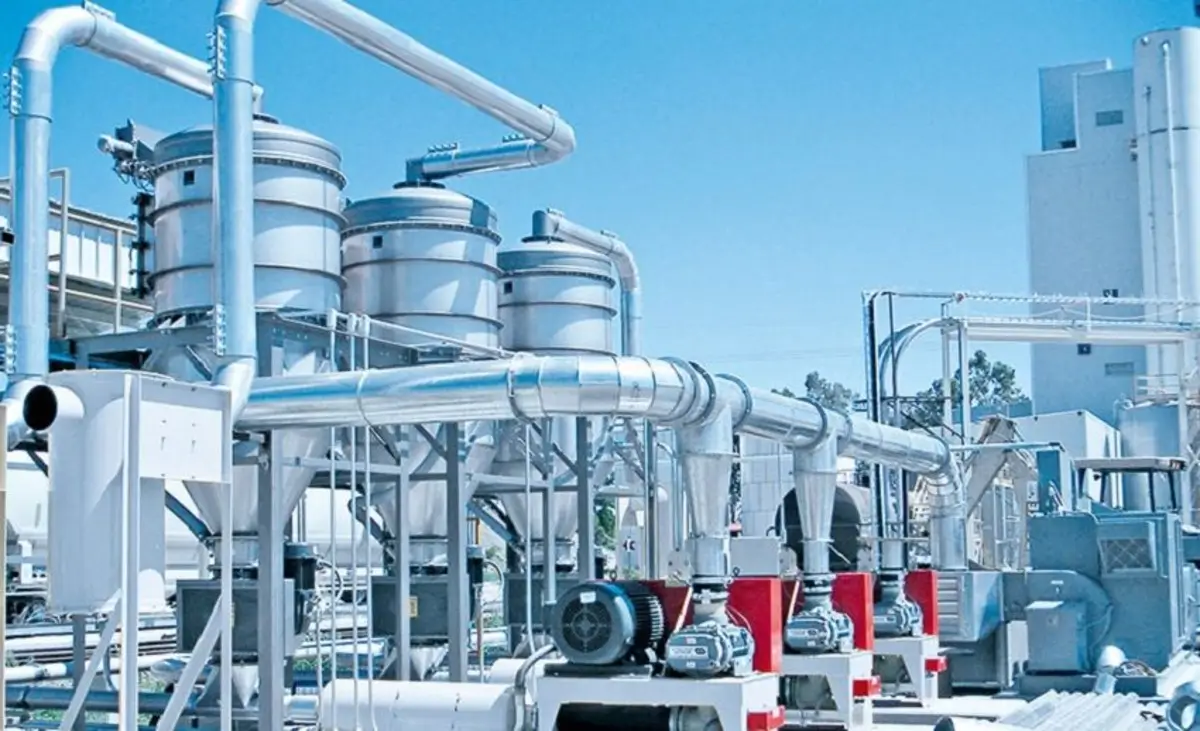
Particle attrition and abrasion caused by industrial transport of bulk solids

Attrition and abrasion in industrial transport

How conveying route, velocity and repeated handling turn intact granules into fines, and how to quantify it.

Dust explosion risk assessment in a chemical powder handling plant

Dust explosion risks and safety protocols

Where combustible dust risk comes from in normal handling, and which powder properties drive the assessment.

Define the powder operating window

A powder can meet specifications and still fail when humidity, consolidation, aeration, temperature, or residence time exceeds its reliable operating conditions.

Choose the test that matches the question

Flow tests answer different questions. Match the method to the process condition, stress state and failure mode instead of treating flowability as one universal property.

Know when the fine fraction takes over

A small increase in fines changes cohesion, air retention, dust formation, packing and segregation even when the median particle size barely moves.

Watch moisture before visible changes appear

Moisture alters cohesion, caking, surface condition, dissolution, flow behavior, and storage stability long before anything looks visibly wet in normal handling.

FAQ

Chemical powder behavior questions

The most important distinction is usually not the visible symptom itself but the mechanism behind it. Similar problems can result from moisture uptake, cohesion, aeration, segregation, attrition, electrostatic effects, or interaction with the equipment and process conditions.
Powder behavior depends on the conditions acting on the material. Humidity, consolidation time, aeration, vibration, temperature, handling history, and stress state can all shift how the same powder flows, cakes, feeds, segregates, or generates dust.
The useful method depends on the question being investigated. Particle size analysis may help with fines or segregation, while shear testing, wall friction, moisture analysis, permeability, dustiness, electrostatic testing, or attrition testing answer different process questions. A useful test programme starts with the suspected mechanism rather than a standard list of measurements.
Start with the information you already have. Use the material route when the powder class is known, the behavior route when a visible symptom is driving the investigation, and the measurement route when you need to decide which test can answer a specific process question.
Laboratory testing is most useful when the symptom alone does not reveal the controlling mechanism, when several causes are plausible, or when a process change needs to be evaluated before implementation. The test conditions should reflect the actual material history and process conditions as closely as practical.
Yes. A visible symptom such as unstable feeding or caking can result from several interacting factors. Combining complementary measurements can help separate effects such as moisture sensitivity, cohesion, bulk density variation, permeability, particle size, or electrostatic behavior.

Need the measurement, not just the guidance? PowderTechnology.info works closely with Delft Solids Solutions,
a contract research organization specializing in the physical behavior of powders and granules. DSS provides
contract testing and characterization, with its laboratory working in accordance with ISO 17025.
Contact Delft Solids Solutions.
Delft Solids Solutions logo