Updated: November 7, 2026
Table of contents

An RNA-loaded lipid nanoparticle may survive drying with its original size and encapsulation efficiency intact, yet the resulting powder may disperse poorly from an inhaler. Conversely, a powder can have excellent aerodynamic properties while its RNA carriers have lost biological activity.
These outcomes arise because drying creates a structure at two different length scales. Nanoparticles, typically around 100 nm, become embedded in larger solid particles containing sugars, amino acids, or other excipients. The manufacturing process determines both the condition of the nanoparticles and the physical structure of their carrier powder.
The engineering task is to control these properties together. Recent research provides evidence about the stresses involved, the mechanisms responsible, and the measurements needed to identify process failures.
Why Convert RNA-LNPs Into Dry Powders?
Lipid nanoparticles protect and transport therapeutic RNA, including small interfering RNA (siRNA) and messenger RNA (mRNA). Approved applications include the siRNA medicine Onpattro and several mRNA vaccines.
Storage requirements vary between products. Onpattro is stored under refrigeration, while several mRNA vaccines have relied on frozen storage to maintain stability. Developing stable dry formulations could simplify distribution, reduce cold-chain dependence, and support different administration routes.
Water contributes to RNA degradation through hydrolysis of the phosphodiester backbone. Lipid oxidation and changes in nanoparticle structure introduce further stability concerns. Removing water slows several degradation pathways, while immobilizing the formulation within an amorphous matrix restricts molecular motion [4].
A lyophilized herpes zoster mRNA vaccine candidate demonstrated the potential benefit. The formulation maintained stability during extended refrigerated storage and produced immune responses in mice comparable to its frozen liquid counterpart [1].
Pulmonary administration creates another reason to develop dry powders. Local delivery could provide access to tissues beyond the liver, a major target of established siRNA therapies.
The lungs can receive RNA-LNPs through nebulized liquid aerosols or inhalable dry powders. Dry powder delivery offers potential advantages in storage, portability, and device operation, but introduces additional requirements for powder dispersion and aerodynamic particle size.
The Two Particle Sizes That Determine Performance
A dry RNA-LNP formulation contains two distinct particle populations.
The first consists of the RNA-loaded lipid nanoparticles. These nanoscale carriers must preserve their structure during processing and retain the ability to deliver functional RNA.
The second consists of the much larger dry powder particles formed during drying. Their geometric size, density, morphology, and interparticle interactions determine how the powder handles, disperses, and behaves in an aerosol.
Why Geometric Size Does Not Equal Aerodynamic Size
For particles in the continuum-flow approximation, aerodynamic diameter can be expressed as [15]:
dₐₑ ≈ d_g × √[ρ_eff / (ρ₀ × χ)]
Where:
- dₐₑ = aerodynamic diameter
- d_g = geometric equivalent-volume diameter
- ρ_eff = effective particle envelope density, accounting for internal voids
- ρ₀ = reference density of 1 g/cm³
- χ = dynamic shape factor, equal to 1 for a sphere
The effective density represents particle mass relative to its envelope volume. Shape is treated separately through χ, avoiding double-counting its influence.
Consider a porous particle with a geometric diameter of 8 µm, an effective density of 0.20 g/cm³, and a dynamic shape factor of 1.2.
Its approximate aerodynamic diameter is:
dₐₑ ≈ 8 × √[0.20 / (1.0 × 1.2)] = 3.3 µm
The particle is geometrically larger than the conventional 1–5 µm respirable range, but its low density gives it an aerodynamic diameter within that range.
The approximation neglects the Cunningham slip correction. For particles of this size, the correction is relatively small and does not alter the engineering conclusion.
This relationship explains why low-density, porous particles can be useful for inhalation. It also shows why process-induced changes in density and morphology matter as much as geometric particle size.
Actual aerosol performance must still be determined experimentally, because particle cohesion and dispersion from the device influence the delivered aerodynamic size distribution.
How Drying Processes Change Particle Structure
Three routes dominate current RNA-LNP powder research: spray drying, lyophilization, and spray-freeze-drying.
Each uses a different mechanism to remove water, creating distinct stresses and powder structures.
Spray Drying: Evaporation, Diffusion, and Shell Formation
Spray drying atomizes an RNA-LNP suspension into droplets and removes solvent through contact with a heated gas stream.
The equipment can operate continuously, but the formulation experiences mechanical stresses during atomization and changes in temperature, concentration, and interfacial area during drying.
The final particle morphology depends strongly on the competition between evaporation and the movement of dissolved or suspended components within each droplet.
This competition is described by the Péclet number (Pe). Following the formulation used by Vehring [14]:
Peᵢ = κ / (8Dᵢ)
Where:
- Peᵢ = Péclet number for component i
- κ = evaporation-rate constant in the droplet diameter-squared law
- Dᵢ = diffusion coefficient of component i
The evaporation-rate constant is defined through the approximate droplet drying relationship:
d(t)² = d₀² − κt
Here, d₀ is the initial droplet diameter and d(t) is its diameter at time t.
The Péclet number compares evaporation-driven surface recession with redistribution by diffusion.
When Pe is below approximately 1, diffusion can redistribute the component throughout the shrinking droplet. More uniform concentration profiles tend to favor relatively dense, homogeneous particles.
When Pe exceeds approximately 1, the receding liquid surface moves faster than the component can redistribute. Material accumulates near the surface, where it may form a solid or highly viscous shell.
The resulting morphology depends on how rapidly that shell forms and how it responds to continued solvent loss. A mechanically stable shell can preserve a hollow particle, while a weaker shell may buckle, wrinkle, or collapse.
For RNA-LNP formulations, the relevant diffusion coefficients differ between dissolved sugars, amino acids, and suspended nanoparticles. Consequently, process settings and excipient composition determine which components become enriched at the surface.
The Péclet framework connects drying conditions directly to the density and morphology used in the aerodynamic diameter equation.
Why Leucine Improves Powder Dispersibility
Leucine is widely used in spray-dried inhalation formulations because it can preferentially accumulate and precipitate near the droplet surface.
Its relatively low solubility and crystallization behavior promote formation of a surface-enriched layer. This can produce corrugated particles with reduced contact area and weaker interparticle cohesion, improving powder dispersion [14, 16].
Sarode and colleagues [7] demonstrated the value of combining leucine with mannitol in spray-dried mRNA-LNP formulations. Their research showed improvements in powder characteristics and successful delivery of functional mRNA following intratracheal administration in mice.
The study also illustrates the importance of processing temperature and solvent composition.
Using a laboratory spray dryer, the researchers compared the following conditions:
| Process condition | Water-based feed | Feed containing 20% ethanol |
|---|---|---|
| Inlet temperature | 90 °C | 60–65 °C |
| Outlet temperature | 46–50 °C | 28–35 °C |
| Aspirator setting | 85% | 85–100% |
| Pump setting | 25% | 15–25% |
Reported laboratory operating conditions from Sarode et al. [7], not general process specifications.
The hydroalcoholic feed permitted lower drying temperatures and reduced powder deposition within the equipment. Changes in leucine and mannitol composition also altered particle morphology and formulation performance.
The inlet temperature alone does not describe the thermal exposure of an LNP. Outlet temperature, feed rate, gas flow, residence time, and solvent evaporation all influence the particle’s thermal history.
Atomizer type, nozzle geometry, atomizing pressure where applicable, and droplet-size distribution also affect mechanical stress and the rate of drying.
For further process context, see PTI’s Modern Spray Drying: Methods and Limitations and the Process and Equipment hub.
Protecting LNPs Against Atomization Stress
The mechanical and interfacial stresses associated with atomization can disrupt lipid structures and release encapsulated RNA.
Farinha and colleagues [3] investigated these stresses in RNA-loaded LNPs and identified poloxamer 188 as an effective protective component under their tested conditions.
The formulation additive helped preserve LNP properties during spray drying by reducing damage associated with atomization.
A useful development experiment separates atomization from drying. Pass the formulation through the selected nozzle, collect the liquid before substantial drying, and compare nanoparticle size and encapsulation efficiency with the original feed.
This identifies the damage caused by droplet formation before changes introduced by evaporation are added. The same approach can be used to compare nozzle settings, atomization energy, and protective additives without changing the entire drying process simultaneously.
Lipid Composition Determines Processing Resistance
The nanoparticle formulation itself also influences spray-drying performance.
Martini and colleagues [9] investigated four siRNA-LNP formulations differing in PEG-lipid and helper-lipid content. Their results showed that these compositional differences affected membrane organization, colloidal stability, and structural changes during spray drying in a lactose matrix.
The findings establish lipid composition as a process variable rather than merely a drug-delivery design choice. A drying process optimized for one LNP formulation cannot be transferred to another without checking the response of its lipid membrane.
Can Spray-Dried RNA-LNPs Retain Biological Activity?
Zimmermann and colleagues [5] demonstrated a spray-dried siRNA-LNP formulation that combined nanoparticle preservation, aerodynamic performance, and biological activity.
The researchers used a 5% w/v lactose solution, with development targets of approximately 150 nm LNP diameter after redispersion, residual moisture below 5%, and RNA loss below 15%. The resulting powders met aerodynamic criteria for delivery to the lower respiratory tract.
Importantly, the siRNA remained functional. The spray-dried LNPs achieved more than 90% protein downregulation in a lung adenocarcinoma cell line and up to 50% gene silencing in ex vivo human precision-cut lung slices.
The work connects process design to the final biological requirement: the powder must disperse into the intended respiratory region while retaining nanoparticles capable of delivering functional RNA.
Friis and colleagues [8] subsequently demonstrated spray drying of mRNA-LNP formulations with retained functionality. Following intratracheal administration in rats, the dried formulations delivered mRNA that produced reporter protein in several pulmonary cell types, including bronchiolar epithelial cells, macrophages, and type II pneumocytes.
Together, these results show that spray drying can produce biologically active RNA-LNP formulations when lipid composition, excipients, and processing conditions are selected appropriately.
Lyophilization: Freezing, Concentration, and Dehydration
Lyophilization removes water from frozen formulations through sublimation under reduced pressure. It avoids the heated gas exposure associated with spray drying, but introduces stresses during freezing and dehydration.
As ice crystals form, RNA-LNPs and dissolved excipients become concentrated in the remaining unfrozen liquid. This cryoconcentration changes local ionic strength, pH, and interactions between nanoparticles.
Ice interfaces and increasing solute concentrations can destabilize lipid structures. During drying, removal of the hydration layer creates additional stress.
Wang and colleagues [10] screened 15 mRNA-LNP formulations and developed a sucrose-containing lyophilized formulation with improved stability and transfection efficiency.
Buffer selection is another important variable. In a continuous freeze-drying study, Meulewaeter and colleagues [13] compared mRNA-LNP formulations containing Tris, phosphate, and phosphate-buffered saline (PBS).
Tris and phosphate were compatible with the investigated formulations, whereas PBS produced less favorable outcomes. Electron microscopy showed that buffer composition influenced LNP morphology before and after lyophilization.
The researchers also found that lipid-to-mRNA ratio influenced RNA retention.
These observations link buffer chemistry to structural changes occurring during freezing. Buffer species, concentration, pH, ionic strength, and lipid composition should be recorded together when comparing formulations.
Lyophilization usually produces a cake that is subsequently reconstituted. Manufacturing an inhalable powder requires additional particle engineering to create the appropriate size, density, and dispersion characteristics.
Spray-Freeze-Drying: Creating Porosity Through Ice Formation
Spray-freeze-drying (SFD) combines atomization with rapid freezing, followed by sublimation of the frozen solvent.
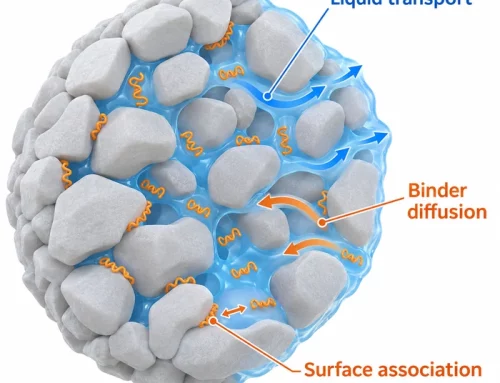
Unlike conventional spray drying, particle formation is not governed primarily by an evaporating liquid surface. Instead, ice nucleation, ice-crystal growth, cryoconcentration, and subsequent sublimation determine much of the powder’s internal structure.
Rapidly frozen droplets can produce highly porous particles because sublimating ice leaves voids within the solid matrix.
Gordon and colleagues [6] demonstrated spray-freeze-dried mRNA-LNP powders with mass median aerodynamic diameters of approximately 3–4 µm and fine particle fractions near 40%.
All four ionizable lipid formulations investigated showed pulmonary mRNA delivery in rats comparable to instilled liquid formulations.
An earlier comparison of polymeric and lipid nanoparticle carriers also demonstrated that spray-freeze-drying could produce highly porous powders, although aerosol performance depended on the carrier system [11].
Why Annealing Changes Encapsulation and Powder Morphology
Arte and colleagues [2] investigated the effect of spray-freeze-drying conditions on RNA-LNP formulations containing sucrose or trehalose.
Their study is particularly useful because it examines nanoparticle properties alongside the physical structure of the dried powder.
The researchers used an ultrasonic nozzle with a feed rate of 2 mL/min and froze the resulting droplets in liquid nitrogen.
The subsequent freeze-drying cycle included:
| Stage | Reported condition |
|---|---|
| Initial shelf temperature | −45 °C |
| Annealing temperature | −15 °C |
| Heating rate to annealing | 0.5 °C/min |
| Annealing hold | 6 hours |
| Primary drying | −31 °C for 48 hours |
| Secondary drying | 30 °C for 8 hours |
| Chamber pressure | 70 mTorr |
These experimental conditions provide a defined basis for comparing annealed and non-annealed formulations.
The Role of the Frozen-Matrix Glass Transition
Annealing is commonly performed above Tg′, the glass transition temperature of the maximally freeze-concentrated formulation, while remaining below conditions that would cause unacceptable melting or structural collapse.
Independent measurements by Horn and Friess [17] provide reference values for the two sugars:
| Freeze-concentrated formulation | Representative Tg′ |
|---|---|
| Sucrose | Approximately −33 °C |
| Trehalose | Approximately −29 to −30 °C |
These values were determined for experimental sugar solutions, not the complete Arte RNA-LNP formulations. Actual Tg′ depends on formulation composition and measurement conditions.
Arte’s −15 °C annealing hold is well above these reference values for both disaccharides.
Above Tg′, the unfrozen concentrated phase gains molecular mobility. Water can migrate between ice crystals, allowing smaller crystals to shrink while larger crystals grow.
This process, known as Ostwald ripening, reduces the total ice-interface area and coarsens the frozen structure.
During subsequent sublimation, larger ice crystals leave larger voids and reduce the internal surface area exposed during drying.
In the Arte study, annealing improved encapsulation stability, particularly in sucrose formulations. The researchers attributed this benefit partly to the reduction in interfacial stress during drying.
However, the same annealing treatment changed the solid powder structure.
Non-annealed formulations produced predominantly spherical, porous particles. Annealed samples developed larger, sheet-like structures, with specific surface areas approximately 10 to 50 times lower than their non-annealed counterparts.
The dry particle-size distributions also shifted upward, with substantially larger coarse-particle fractions after annealing.
The reduction in BET surface area confirms major changes in the accessible pore structure. It provides a reason to investigate whether effective density and aerodynamic behavior have changed.
This is the central process trade-off: annealing can protect nanoscale LNPs while changing the micrometer-scale carrier particles that determine powder handling and delivery.
Choosing Excipients: Protection Is Not the Only Requirement
Sucrose and trehalose protect lipid nanoparticles partly by replacing interactions normally provided by water and forming an amorphous matrix around the particles.
Their performance depends on concentration, moisture content, processing history, and the ability of the dried matrix to remain amorphous.
Sugar Loading Must Be Related to Lipid Content
In the Arte study [2], sucrose and trehalose were tested at 2.5%, 5%, 10%, and 20% w/v in the liquid feed.
These concentrations are useful process descriptors, but they do not independently establish how much protectant surrounds each LNP.
A more informative formulation comparison also reports sugar-to-lipid mass ratio.
The study used a nominal RNA-to-lipid mass ratio of 1:17 and diluted the LNP suspension to an RNA concentration of 0.1 mg/mL before adding sugar. Assuming retention of the nominal lipid-to-RNA ratio, the following values can be calculated:
| Feed sugar concentration | Sugar concentration | Nominal sugar-to-lipid mass ratio |
|---|---|---|
| 2.5% w/v | 25 mg/mL | Approximately 15:1 |
| 5% w/v | 50 mg/mL | Approximately 29:1 |
| 10% w/v | 100 mg/mL | Approximately 59:1 |
| 20% w/v | 200 mg/mL | Approximately 118:1 |
Calculated nominal ratios from the reported feed composition, not independently measured lipid concentrations.
This distinction becomes important when LNP concentration changes during development or scale-up. Two feeds with the same sugar concentration can have different sugar-to-lipid ratios and therefore different protective capacity.
Higher loading also changes feed viscosity, total solids, particle formation, and the amount of excipient delivered with the RNA.
Why Sucrose and Trehalose Behave Differently
Trehalose has a higher dry-state glass transition temperature than sucrose. Representative values for dry amorphous materials are approximately 110–115 °C for trehalose and 65–75 °C for sucrose, with measured values affected by moisture content and composition.
A higher glass transition temperature generally favors physical stability by restricting molecular mobility during storage.
Yet trehalose did not perform better in the Arte experiments.
The annealed 20% trehalose formulation showed evidence of trehalose dihydrate crystallization, increased residual moisture, and less favorable encapsulation results.
Crystallization reduces the amorphous material available to stabilize nanoparticles. Formation of the hydrated crystalline phase also alters water retention and the efficiency of moisture removal.
The sucrose formulations remained predominantly amorphous under the investigated conditions and provided better encapsulation stability during the eight-week storage study.
The result illustrates why the glass transition temperature of the dry sugar cannot be used alone to rank formulation performance. Crystallization behavior and the actual freeze-drying cycle determine whether the protective amorphous phase survives.
Why Moisture Content and Glass Transition Are Linked
Water plasticizes amorphous carbohydrate matrices. As residual moisture increases, molecular mobility rises and the glass transition temperature decreases.
The Gordon–Taylor relationship describes this effect by linking the glass transition temperature of a mixture to the mass fractions and properties of its components.
Consequently, residual moisture and storage temperature must be considered together.
Targets such as residual moisture below 2% and a glass transition temperature at least 20 °C above storage temperature describe related aspects of the same physical stability requirement [4].
The moisture concentration determines, in part, the glass transition temperature of the solid matrix. That temperature then influences whether the formulation remains in a stable glassy state during storage.
A moisture measurement should therefore be interpreted alongside thermal analysis and moisture-sorption behavior.
Why Sucrose Stability Does Not Guarantee Inhaler Performance
Sucrose has an important disadvantage in dry powder inhalation formulations: its hygroscopicity and tendency toward deliquescence under sufficiently humid conditions.
Water uptake can lower the glass transition temperature, increase particle adhesion, and promote caking or poor powder dispersion.
This creates a different formulation requirement from that of a sealed product intended for reconstitution.
Ogawa and colleagues [12] investigated pH-modified spray-freeze-drying to produce inhalable mRNA-LNP powders without relying on deliquescent excipients.
By modifying formulation pH, the researchers strengthened interactions between mRNA and ionizable lipids, improving RNA retention during processing. The resulting powders demonstrated aerosol performance and biological activity in experimental systems.
This provides an alternative strategy when the excipient needed for nanoparticle protection compromises powder handling or aerosolization.
Diagnosing RNA-LNP Powder Failures
A final powder measurement cannot reveal which processing stage caused a defect. The investigation should separate atomization, freezing, drying, and storage wherever possible.
The following matrix connects observable changes to likely mechanisms and the first useful diagnostic experiment.
| Observed problem | Mechanism to investigate | Discriminating measurement | Candidate adjustment after confirmation |
|---|---|---|---|
| Encapsulation efficiency falls while LNP size remains stable | Atomization: interfacial and mechanical stress | Encapsulation before and after an atomization-only run | Screen poloxamer 188 and reduce damaging atomization conditions |
| LNP size increases while encapsulation remains stable | Freezing: cryoconcentration or ice-interface stress | DLS after a freeze-thaw-only control | Increase protectant loading and compare sucrose with trehalose |
| Size and encapsulation deteriorate after drying | Dehydration: loss of hydration forces and matrix protection | Compare post-freezing and post-drying samples | Change protectant ratio and drying cycle |
| Encapsulation deteriorates during storage | Solid state: crystallization, moisture uptake, or matrix mobility | XRPD, Karl Fischer, and thermal analysis | Preserve the amorphous phase and reduce moisture exposure |
| Good LNP stability but poor fine particle fraction | Particle formation: unfavorable density, morphology, or cohesion | Aerodynamic testing, SEM, density, and particle-size distribution | Adjust atomization, solids loading, leucine content, or freezing conditions |
| Powder cakes or disperses poorly after humidity exposure | Storage and handling: moisture plasticization and increased cohesion | Dynamic vapor sorption, glass transition, and aerosol testing | Reduce hygroscopic excipient exposure, improve packaging, or change excipient system |
| LNP size and encapsulation pass, but biological activity falls | RNA or lipid damage not captured by physical measurements | RNA integrity and functional transfection assay | Investigate RNA degradation, lipid chemistry, and delivery functionality |
Use the stage-specific control to identify the first failure before changing multiple formulation variables.
For example, if encapsulation decreases immediately after atomization, changing the freeze-drying shelf temperature is unlikely to address the initiating mechanism.
Likewise, if a powder passes the immediate post-drying tests but fails after humid storage, the investigation should begin with moisture uptake, crystallinity, and matrix mobility.
Reconstitution failures may also involve poor wetting or incomplete agglomerate breakup rather than damaged nanoparticles. PTI’s wetting, dispersion, and dissolution troubleshooting guide explains how to separate these mechanisms.
What Should Be Measured Before Selecting a Process?
A useful characterization program connects each critical quality attribute to a mechanism and a product decision.
The measurements must distinguish the condition of the dry powder from the integrity of the RNA-loaded nanoparticles after reconstitution.
Match Each Technique to the Question It Can Answer
| Technique | What it reveals | What it cannot establish |
|---|---|---|
| Karl Fischer titration | Residual water content after drying | Long-term storage stability or matrix mobility |
| Laser diffraction and SEM | Geometric particle-size distribution, morphology, and visible agglomeration | Aerodynamic deposition or RNA-LNP integrity |
| BET surface area | Accessible specific surface area and changes associated with porosity | Effective particle density or aerosol dispersibility |
| XRPD and thermal analysis | Crystallinity, phase transitions, and glass transition behavior | RNA integrity or biological activity |
| DLS after reconstitution | LNP hydrodynamic size, polydispersity, and aggregation | RNA encapsulation, molecular integrity, or functionality |
| Cascade impactor testing | Aerodynamic particle-size distribution, MMAD, and fine particle fraction | Nanoparticle integrity after deposition or biological activity |
Technique selection depends on the intended product and the failure mechanism being investigated.
The distinction between geometric and aerodynamic particle size is particularly important for inhalable powders. Laser diffraction and imaging provide information about particle size and shape, while cascade impactor testing establishes aerodynamic behavior under defined conditions.
Likewise, BET surface area can show that annealing has changed the accessible pore structure, but the measurement does not directly determine the emitted dose or fine particle fraction.
PTI’s particle size and morphology, density, packing, porosity, and surface area, and moisture and environmental response guides provide further measurement context.
Measurements After Reconstitution
Dry powder characterization must be complemented by tests of the recovered nanoparticles.
Dynamic light scattering measures changes in hydrodynamic particle size and polydispersity. Encapsulation assays determine how much RNA remains associated with or protected within the LNP system.
RNA integrity measurements establish whether the nucleic acid has undergone degradation. A relevant biological assay then confirms whether the formulation retains its intended activity.
These measurements address different failure modes. A formulation with unchanged particle size can still have reduced encapsulation efficiency, while a formulation with acceptable encapsulation may contain damaged RNA.
For inhalable products, emitted dose and dose uniformity are also required because an aerodynamically suitable formulation may disperse inconsistently from the delivery device.
Development Targets and Screening Criteria
Published studies provide useful starting points for experimental design. Product acceptance criteria must ultimately reflect the intended administration route, stability requirements, and analytical variability.
| Attribute | Reference point or proposed screening target | Basis |
|---|---|---|
| Mass median aerodynamic diameter | Approximately 3–4 µm for the investigated inhalation formulations | Reported by Gordon et al. [6] |
| Fine particle fraction | Approximately 40% as a published performance benchmark | Reported by Gordon et al. [6] |
| Residual moisture | Below 5% as a formulation target; below 2% as a more demanding stability-oriented starting point | Zimmermann et al. [5]; review [4] |
| Glass transition margin | At least 20 °C above intended storage temperature | Stability guidance discussed in [4] |
| LNP size after reconstitution | No more than 1.2 times the initial diameter | Proposed early-development screening criterion |
| Encapsulation efficiency loss | No more than 5 percentage points relative to the initial feed | Proposed early-development screening criterion |
| RNA integrity | No unacceptable change relative to the reference formulation | Product-specific analytical requirement |
| Biological activity | Retention of the intended functional response | Product-specific assay requirement |
The two proposed numerical screening limits are engineering starting points, not regulatory standards or values established by the cited studies. They should be adjusted using assay precision, formulation variability, and required biological performance.
The MMAD and FPF figures are experimental benchmarks rather than universal inhalation specifications. Their interpretation depends on the delivery device, test conditions, aerodynamic cutoff, and intended deposition region.
For formulation development, the most informative result is often the change between controlled processing stages.
A small increase in LNP size during atomization points toward a different intervention than a larger increase occurring only after freezing. Similarly, poor aerodynamic performance requires investigation of particle formation and dispersion rather than further optimization of encapsulation alone.
Limits of the Current Evidence
The studies reviewed here establish several viable routes to dry RNA-LNP formulations, but most biological results come from model RNA, reporter mRNA, siRNA, cultured cells, tissue systems, or animal experiments.
The Arte spray-freeze-drying study [2] used model yeast RNA and measured nanoparticle properties and powder stability. It did not evaluate aerosol performance or functional RNA delivery.
Other studies demonstrated biological activity after pulmonary administration in rodents, but these results do not establish equivalent clinical performance in humans.
Long-term ambient stability also remains insufficiently demonstrated for most mRNA therapeutics outside vaccine applications [4].
Finally, none of the studies reviewed here established the dry-powder performance of a complete gene-editing payload containing components such as Cas9 mRNA and guide RNA. The demonstrated findings concern RNA-LNP processing, physical stability, and selected RNA delivery applications.
Conclusion: Select the Process Against Both Particle Scales
RNA-LNP powder development requires control of two related but distinct structures: the nanoscale lipid carrier and the larger dry powder particle.
The drying route determines the stresses imposed on the nanoparticles, while atomization, evaporation, freezing, and matrix formation determine the properties of the resulting powder.
The Péclet number provides a framework for understanding shell formation during spray drying. Freeze-concentrated matrix behavior and ice-crystal growth explain the changes produced by annealing during spray-freeze-drying. Aerodynamic diameter links geometric size, effective density, and particle shape to inhalation performance.
These mechanisms also explain why improving one property can create a problem elsewhere. A higher sugar loading may protect encapsulation but alter powder structure. Annealing may reduce interfacial damage while coarsening particles. A stable sucrose matrix may preserve LNP properties while remaining sensitive to humidity during inhaler use.
The most effective development strategy is to identify the stage responsible for each change, select measurements that distinguish the mechanisms, and then adjust formulation and process variables against the complete product requirement.
Frequently asked questions
References
- Munoz-Moreno R, et al. A highly stable lyophilized mRNA vaccine for Herpes Zoster provides potent cellular and humoral responses. npj Vaccines. 2025;10:49.
- Arte KS, et al. Spray Freeze Drying for Solid Formulations of RNA Lipid Nanoparticles. AAPS PharmSciTech. 2026;27:284.
- Farinha S, et al. Mitigating Shear Stress in Spray Drying for RNA-Loaded Lipid Nanoparticles through Process and Formulation Optimization. AAPS PharmSciTech. 2025;26:145.
- El-Tanani M, et al. Ambient-Stable mRNA Medicines: Emerging Paradigms in Dry and Solid-State Formulation. Pharmaceuticals. 2026;19(3):370.
- Zimmermann CM, et al. Spray drying siRNA-lipid nanoparticles for dry powder pulmonary delivery. Journal of Controlled Release. 2022;351:137–150.
- Gordon A, Li B, Witten J, Nguyen H, Anderson DG. Inhalable Dry Powders for Lung mRNA Delivery. Advanced Healthcare Materials. 2024;13(29).
- Sarode A, et al. Inhalable dry powder product (DPP) of mRNA lipid nanoparticles (LNPs) for pulmonary delivery. Drug Delivery and Translational Research. 2024;14(2):360–372.
- Friis KP, et al. Spray dried lipid nanoparticle formulations enable intratracheal delivery of mRNA. Journal of Controlled Release. 2023;363:389–401.
- Martini N, et al. Understanding excipient interactions unlocks untapped potential of RNA-lipid nanoparticles in dry powder formulations for local pulmonary delivery. Journal of Controlled Release. 2026;390:114539.
- Wang T, et al. Development of lyophilized mRNA-LNPs with high stability and transfection efficiency in specific cells and tissues. Regenerative Biomaterials. 2025;12.
- Ali ME, Lamprecht A. Spray freeze drying for dry powder inhalation of nanoparticles. European Journal of Pharmaceutics and Biopharmaceutics. 2014;87(3):510–517.
- Ogawa K, et al. Stable and inhalable powder formulation of mRNA-LNPs using pH-modified spray-freeze drying. International Journal of Pharmaceutics. 2024;665:124632.
- Meulewaeter S, et al. Continuous freeze-drying of messenger RNA lipid nanoparticles enables storage at higher temperatures. Journal of Controlled Release. 2023;357:149–160.
- Vehring R. Pharmaceutical Particle Engineering via Spray Drying. Pharmaceutical Research. 2008;25(5):999–1022.
- Finlay WH. The Mechanics of Inhaled Pharmaceutical Aerosols: An Introduction. 2nd ed. Academic Press; 2019.
- Lechanteur A, Evrard B. Influence of Composition and Spray-Drying Process Parameters on Carrier-Free DPI Properties and Behaviors in the Lung: A Review. Pharmaceutics. 2020;12(1):55.
- Horn J, Friess W. Detection of Collapse and Crystallization of Saccharide, Protein, and Mannitol Formulations by Optical Fibers in Lyophilization. Frontiers in Chemistry. 2018;6:4.