Updated: November 7, 2026
Table of contents
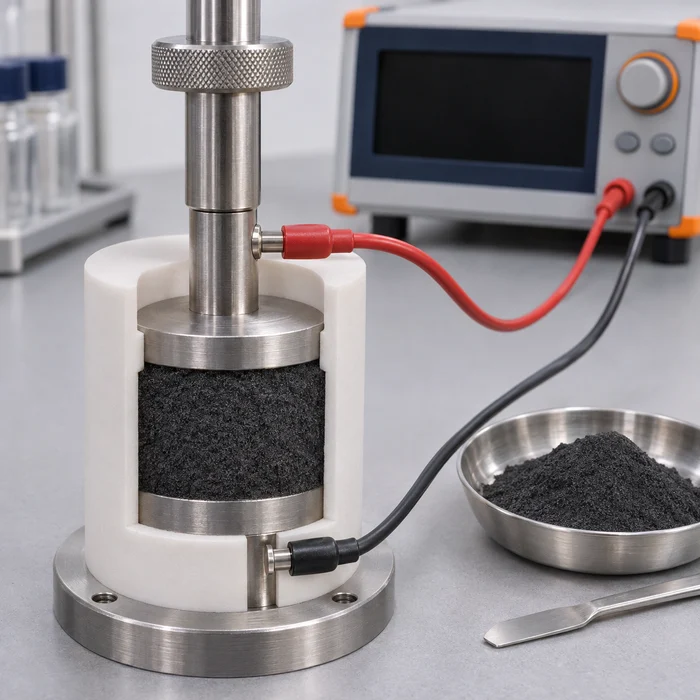
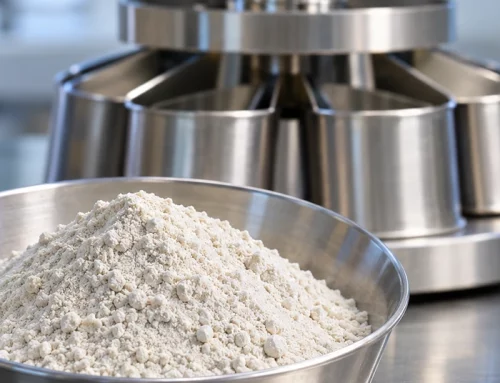
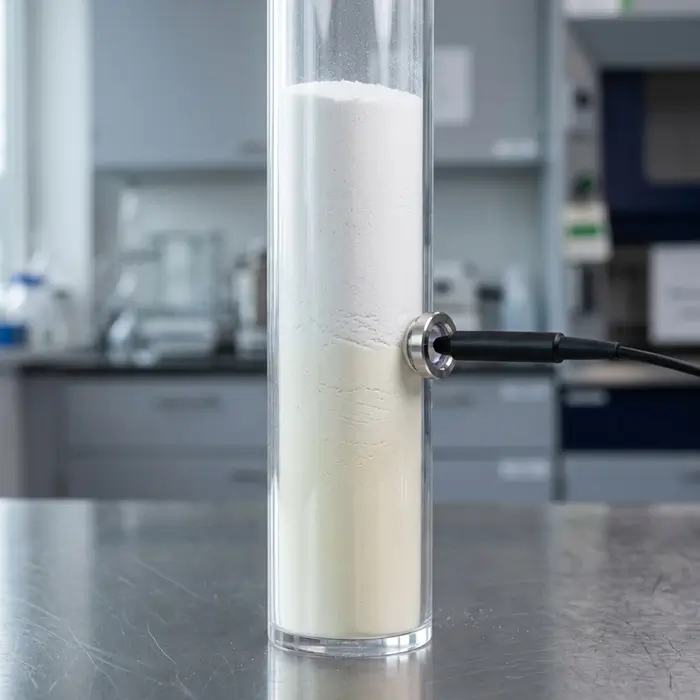
Conceptual cutaway of powder-bed resistance measurement. Packing and particle contacts influence the electrical path through the bed.
A stainless steel hopper may be properly grounded while powder inside it remains charged. Similarly, adding conductive filler to a blend does not guarantee an electrical path through the material. In both cases, an individual particle’s conductivity tells only part of the story.
The distinction matters when diagnosing powder adhesion, feeding problems, electrostatic coating defects, and ignition hazards. Several studies discussed below examine contacts or conductive networks in adjacent material systems. They help explain the mechanisms; their numerical results should not be treated as universal powder specifications.
What Does Electrical Conductivity Mean for a Powder?
Electrical conductivity, σ, describes how readily current passes through a material and is measured in siemens per meter (S/m). Volume resistivity, ρ, describes opposition to current and is measured in ohm-meters (Ω·m). For an ohmic material under the same conditions, σ = 1/ρ.
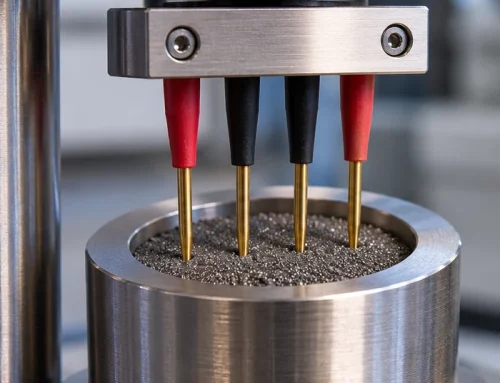
A powder bed is a network of particles and contacts rather than a solid block. Its measured resistivity depends on preparation and test conditions. Report the electrode arrangement, bed density or applied pressure, temperature, humidity, and test method. A value for solid metal or polymer cannot simply be assigned to a bed of its particles.
IEC TS 60079-32-1 classifies bulk powders by volume resistivity for electrostatic-hazard assessment [1]:
| Powder class | Bulk volume resistivity, ρ |
|---|---|
| Low resistivity | ρ ≤ 10⁶ Ω·m |
| Medium resistivity | 10⁶ Ω·m < ρ ≤ 10¹⁰ Ω·m |
| High resistivity | ρ > 10¹⁰ Ω·m |
These are resistivity categories, not safe/unsafe categories. The ignition risk also depends on the charging process, possible discharge types, dust sensitivity, and equipment design. Charge generation during contact and separation is distinct from the rate at which charge subsequently dissipates.
How Do Surface Films Change Interparticle Conduction?
Even highly conductive particles may form a poorly conducting bed if electrical contact is interrupted. Thin oxides, deposits, or additives on particle surfaces can raise contact resistance. IEC electrostatic guidance notes that oxide films can prevent metal powders from retaining low bulk resistivity [1]. Contact pressure and consolidation can also change the result.
In experiments on silver-plated electrical contacts, Alderete and colleagues found that a silver sulfide (Ag₂S) tarnish film increased contact resistance by more than a factor of ten at applied loads of 5 N or less. At higher loads, the film could be punctured, reducing its influence [2]. The underlying mechanism matters for powder contacts: a conductive core does not guarantee a low-resistance connection to the next particle.
When a powder’s resistivity changes between batches, investigate surface condition and packing before attributing the difference to the parent material. Temperature and moisture history should be recorded as possible influences on both the material and its contacts.
Why Do Particle Contacts and Packing Control Conductivity?
Current through a powder bed must cross many contacts. Compression can increase their number or effective area, although the response depends on particle shape, deformation, and surface chemistry.
Marinho and colleagues compared compacts of graphene, multiwall carbon nanotubes, carbon black, and graphite. Under 5 MPa of applied pressure, graphite reached approximately 10³ S/m, versus about 10² S/m for the other three materials. Conductivity reflected packing and contacts as well as the parent material [3]. For engineering comparisons, consolidation pressure must accompany the conductivity result.
When Does Conductive Filler Form a Connected Network?
In a blend of conducting and insulating particles, long-range electrical transport emerges when the conducting particles form a connected network. This transition is called electrical percolation.
Ziff and Torquato modeled maximally random jammed packings of equal-sized spheres. The threshold occurred when approximately 31.16% of the spheres were conducting. Because the bed included voids, those conducting spheres occupied approximately 19.9% of the entire bed volume at the threshold [4]. These percentages have different denominators and should not be interchanged.
Barbieri and colleagues modeled conducting spherical fillers within an insulating polymer matrix. Their percolation threshold was about 23.5% filler by volume for a homogeneous distribution and approached 4% when the conducting phase was segregated into connected regions [5]. Together, these results demonstrate why geometry and distribution matter more than a fixed recipe percentage.
For a new conductive formulation, measure resistivity over a filler concentration series. Repeat measurements at the packing pressures and moisture conditions encountered during use. A mixture may pass a conductivity target when compressed but fail it when loosely packed.
How Does Humidity Influence Charging?
Adsorbed water can provide additional pathways for charge leakage along particle surfaces. However, moisture can also increase cohesion and change powder flow. Raising humidity is therefore not automatically a suitable correction for static-related sticking.
Schella and colleagues studied polymer beads shaken in a stainless steel vessel. Charging was pronounced at low relative humidity, generally below 30%, and small above approximately 80%. The transition varied by polymer, while electrostatic attraction also changed the beads’ segregation behavior [6].
If a problem varies between seasons or production shifts, compare powder resistivity and charge-to-mass ratio across the actual humidity range. Also record temperature: heating air without adding water vapor lowers relative humidity and may change surface conduction.
Why Does Charge Persist in a Grounded Hopper?
Particle-to-particle and particle-to-wall contact and separation generate triboelectric charge. Pneumatic conveying is an effective charging process because particles repeatedly contact pipes and one another [7]. Grounding conductive equipment prevents it from remaining electrically isolated, but it does not create a conducting path through every particle in the powder.
For a bulked powder that behaves approximately ohmically, the charge-relaxation time is [1]:
τ = ε₀ εᵣ ρ
Here τ is the relaxation time in seconds; ε₀ is the permittivity of free space, approximately 8.85 × 10⁻¹² F/m; εᵣ is the powder bed’s relative permittivity; and ρ is its bulk volume resistivity in Ω·m. In the ideal exponential model, one relaxation time reduces the initial charge to about 37% of its value, provided a suitable route to ground exists.
With εᵣ = 2, a bed with ρ = 10¹⁰ Ω·m has τ ≈ 0.18 s, while ρ = 10¹² Ω·m gives τ ≈ 17.7 s. That difference can determine whether charge dissipates on the timescale of filling or continues to accumulate. The calculation is an estimate, not an independently validated safe residence time: charged or nonohmic beds, contact limitations, and equipment geometry may behave differently. It does not apply directly to powder suspended in air, where charge loss depends on particle interactions and deposition rather than conduction through a bulk bed [1]. Measure charge decay under process-relevant conditions when the timing matters.
An investigation of pneumatically conveyed wheat flour in plastic silos illustrates the distinction. The tested flour had resistivity below 10⁹ Ω·m and a charge-decay time shorter than 0.1 s. Despite the rapid decay observed for that material, the authors also examined possible discharges associated with insulating silo walls [8]. Their measurements describe the assessed installation, not wheat flour or plastic silos in general.
Electrostatic attraction can also affect wall adhesion, powder handling, and blend uniformity. Chargeability testing on pharmaceutical powders supports assessing electrostatic behavior alongside conventional flow properties [9]. When powders stick or discharge erratically, PTI’s electrostatic troubleshooting guide and shear cell testing guide can help separate charging from mechanical cohesion.
Which Electrostatic Discharges Matter for Combustible Powders?
Electrostatic ignition hazards depend on the discharge mechanism, the atmosphere, and the minimum ignition energy (MIE) of the relevant dust cloud. A low resistivity measurement alone cannot establish that a system is safe [1].
- Spark discharges: An isolated conductor, including a metal part or tool, may accumulate charge and discharge suddenly. Bond and ground suitable conductive equipment.
- Brush discharges: Charged insulating surfaces can produce discharges capable of igniting flammable gases or vapors. In the absence of those gases or vapors, ordinary brush discharges are not generally considered capable of igniting a pure combustible dust cloud. Hybrid atmospheres require separate assessment.
- Cone discharges: A highly charged powder heap forming during silo filling can produce a discharge energetic enough to ignite sensitive dust clouds.
- Propagating brush discharges: Highly charged insulating layers, particularly with conductive backing, can produce very energetic discharges. Evaluate liners, coatings, flexible hoses, and silo wall construction.
- People as isolated conductors: Operators may accumulate charge if footwear and flooring do not provide a suitable path to ground. Where the risk assessment requires electrostatic control, check the footwear and installed floor as a system under operating conditions. IEC 61340-4-3 specifies resistance tests for footwear, and IEC 61340-4-1 covers floor coverings and installed floors [10]. Dirt, coatings, and insulating deposits can interrupt the path to ground; electrical shock hazards must also be considered.
- FIBC types A, B, C, and D: Type A bags have no built-in electrostatic protection. Type B uses nonconductive construction and fabric with an electrical breakdown voltage of 6 kV or less to prevent propagating brush discharges. Because the bag contains no conductive elements, it cannot itself produce a spark, but it does not prevent brush discharges or sparks from other isolated conductors. Do not use Type B where flammable gases or vapors are present or the dust MIE is 3 mJ or less. Type C uses conductive elements and must be grounded before and throughout filling and emptying. Type D provides static protection without a bag-to-ground connection, but nearby conductors and any liner still require assessment. Select the FIBC and liner for the actual dust, MIE, and atmosphere under IEC 61340-4-4 [11].
Assess charge generation, insulating components, grounding paths, dust-cloud formation, ignition sensitivity, and credible discharges together. Controls for a combustible dust atmosphere may also require explosion prevention or protection beyond electrostatic measures.
Which Standards and Regulations Apply?
United States. NFPA 660, Standard for Combustible Dusts and Particulate Solids (2025 edition), became effective as an NFPA standard on December 6, 2024. It consolidated the former NFPA 61, 484, 652, 654, 655, and 664 combustible-dust standards. NFPA 77:2024 addresses static-electricity control [12] [13]. A standard’s legally enforceable status depends on adoption and the relevant authority; NFPA publication alone does not make every requirement law nationwide.
European Union. Directive 2014/34/EU covers equipment and protective systems intended for potentially explosive atmospheres. Directive 1999/92/EC covers worker protection in potentially explosive atmospheres [14].
Great Britain. The Dangerous Substances and Explosive Atmospheres Regulations 2002 (DSEAR) address workplace risks. The Equipment and Protective Systems Intended for Use in Potentially Explosive Atmospheres Regulations 2016 govern relevant products placed on the market [15].
Technical guidance and tests. IEC TS 60079-32-1:2013+A1:2017 gives electrostatic-hazard guidance, and its European publication is CLC/TR 60079-32-1:2018. IEC 60079-32-2:2015 specifies electrostatic test methods, including powder resistivity. IEC 61340-4-4:2018 covers FIBC electrostatic classification and testing [1] [16] [11]. These documents support, rather than replace, a site-specific assessment and applicable legal duties.
How Does Conductivity Affect Electrostatic Powder Coating?
Powder must acquire charge and remain attracted to a grounded workpiece long enough to form a coating. Corona guns, the most widely used approach, charge powder in a high-voltage corona discharge. Tribo guns charge particles through frictional contact inside the gun; their performance depends strongly on powder formulation and its ability to charge by contact [17]. Charging method, humidity, workpiece grounding, and powder properties must therefore be considered together.
US Patent 5,518,546 describes a particular induction/conduction charging approach for modified resin powders. It proposes resistivity of roughly 10⁹ to 10¹³ Ω·m, with a preferred range of 10¹⁰ to 10¹² Ω·m at 20% relative humidity [18]. This is a proposed range for that patented method, not a universal specification for corona or tribo powder coating.
At excessive deposited charge, back ionization can disrupt film formation and leave craters, voids, or star-like patterns. Orange peel has other possible causes, including film thickness, formulation, particle-size distribution, and curing conditions [19]. Inspect gun settings and the coating process rather than diagnosing either defect from appearance alone.
How Should Engineers Measure and Troubleshoot Conductivity?
Begin with the process symptom and choose a measurement that can distinguish charging, retention, and contact-network behavior. IEC 60079-32-2 provides test methods useful in electrostatic hazard assessment, including powder-bed resistivity [16].
| Engineering question | Measurement or check | What to establish |
|---|---|---|
| Why does powder stick after conveying? | Net charge-to-mass ratio using a Faraday pail and electrometer before and after the handling step; sample mass, humidity, and contact materials [20] | Whether handling creates or changes net charge, and where it occurs |
| Why does charge persist after shutdown? | Powder-bed resistivity, estimated τ, and measured charge-decay time | Whether charge can dissipate within the actual process timescale |
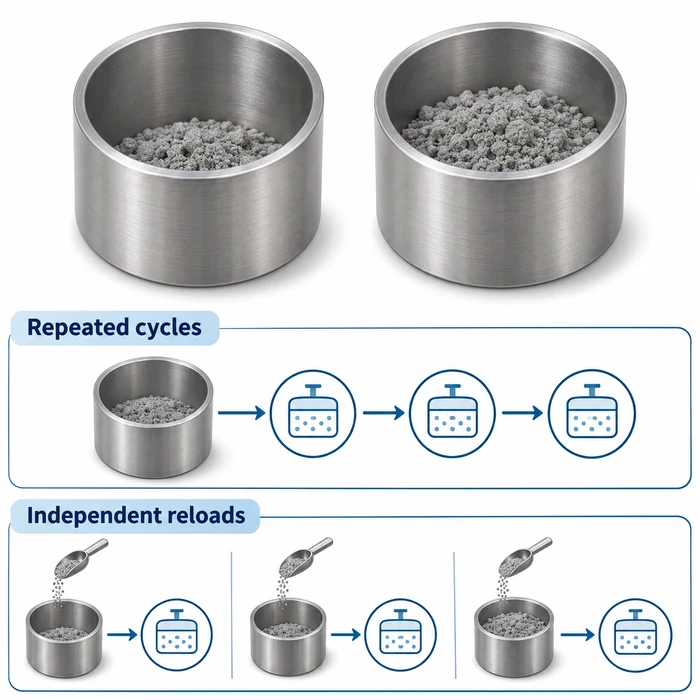
| Why did a conductive blend become resistive? | Bed resistivity versus filler loading, compaction pressure, and packing state | Whether a connected network forms and remains connected |
| Why does coating coverage change? | Gun method and settings, powder charge, substrate grounding, humidity, and film build | Whether charging, deposition, or subsequent film behavior causes the defect |
| Are electrostatic ignition controls adequate? | Hazard assessment of dust MIE, discharge mechanisms, isolated conductors and people, liners, FIBC type, grounding, and protective measures | Whether credible ignition sources are controlled across the installation |
For comparative testing, condition specimens consistently and document their moisture history, temperature, humidity, packing or pressure, and preparation. A charge-to-mass result describes net charge, not the entire distribution of positive and negative charges on particles. Where possible, change one process variable at a time so that a conductivity shift is not confused with a new moisture film or different packing state.
Conclusion
A powder’s electrical response is determined by its particles, their contacts, and the conditions under which the bed forms. Volume resistivity helps estimate charge relaxation in bulked powder, while charge-to-mass measurements show what the handling process generates. Neither measurement alone is a substitute for examining contact networks, equipment grounding, and credible ignition mechanisms.
For troubleshooting, determine where charge is generated, how long it persists, and whether a conductive pathway exists under the actual operating conditions. Those answers can guide adjustments to materials, equipment, and process settings without relying on generic conductivity labels.
Frequently asked questions
References
- IEC. IEC TS 60079-32-1:2013+A1:2017, Explosive atmospheres, Part 32-1: Electrostatic hazards, guidance. International Electrotechnical Commission.
- Alderete B, Mücklich F, Suarez S. Tarnishing (Ag₂S) Layer on Silver-Plated Electrical Contacts: Its Influence on Electrical Contact Resistance. IEEE Transactions on Components, Packaging and Manufacturing Technology. 2023;13(1):45-58.
- Marinho B, Ghislandi M, Tkalya E, Koning CE, de With G. Electrical conductivity of compacts of graphene, multi-wall carbon nanotubes, carbon black, and graphite powder. Powder Technology. 2012;221:351-358.
- Ziff RM, Torquato S. Percolation of disordered jammed sphere packings. Journal of Physics A: Mathematical and Theoretical. 2017;50:085001.
- Barbieri E, Bilotti E, Liu Y, Grimaldi C. Pyroresistive response of percolating conductive polymer composites. Physical Review Materials. 2024;8:045602.
- Schella A, Herminghaus S, Schröter M. Influence of humidity on tribo-electric charging and segregation in shaken granular media. Soft Matter. 2017;13:394-401.
- Matsusaka S, Maruyama H, Matsuyama T, Ghadiri M. Triboelectric charging of powders: A review. Chemical Engineering Science. 2010;65:5781-5807.
- Pavey ID, de Broissia L, Rotchell AK. Assessment of Electrostatic Ignition Hazard in Plastic Silos by Combining Computer Modelling of Electric Fields with Experimental Measurements. Chemical Engineering Transactions. 2019;77:319-324.
- Ramirez-Dorronsoro JC, Jacko RB, Kildsig DO. Chargeability measurements of selected pharmaceutical dry powders to assess their electrostatic charge control capabilities. AAPS PharmSciTech. 2006;7(4):103.
- IEC. IEC 61340-4-3:2017, Electrostatics, Part 4-3: Standard test methods for specific applications – Footwear, and IEC 61340-4-1:2003+A1:2015, Electrostatics, Part 4-1: Standard test methods for specific applications – Electrical resistance of floor coverings and installed floors. International Electrotechnical Commission.
- IEC. IEC 61340-4-4:2018, Electrostatics, Part 4-4: Electrostatic classification of flexible intermediate bulk containers (FIBC). International Electrotechnical Commission.
- NFPA. NFPA 660:2025, Standard for Combustible Dusts and Particulate Solids. National Fire Protection Association.
- NFPA. NFPA 77:2024, Recommended Practice on Static Electricity. National Fire Protection Association.
- European Union. Directive 2014/34/EU (equipment and protective systems) and Directive 1999/92/EC (worker protection in explosive atmospheres).
- UK Health and Safety Executive. ATEX and explosive atmospheres. Guidance on DSEAR and the 2016 EPS Regulations.
- IEC. IEC 60079-32-2:2015, Explosive atmospheres, Part 32-2: Electrostatics hazards, Tests. International Electrotechnical Commission.
- Pélissier K, Thierry D. Powder and High-Solid Coatings as Anticorrosive Solutions for Marine and Offshore Applications? A Review. Coatings. 2020;10(10):916. Review of electrostatic corona and tribo powder application methods.
- US Patent 5,518,546. Apparatus for coating substrates with inductively charged resinous powder particles. Issued May 21, 1996.
- TCI Powder Coatings. Guide to the Application & Troubleshooting of Electrostatic Coatings. Application and troubleshooting guide.
- IEC. IEC TR 61340-2-2:2000, Electrostatics, Part 2-2: Measurement methods – Measurement of chargeability. See Faraday pail measurement procedures.