Updated: November 18, 2026

In Part 2, we explored techniques used to create particles. Here, we focus on micronization and the laws of comminution used to estimate size-reduction energy.
Particle engineering aims to control particle size, size distribution, and surface characteristics to achieve the required product performance. Micronization reduces particles to the low micrometer range, changing properties such as dissolution rate, flow behavior, and texture. These changes are not always beneficial: finer particles can, for example, become more cohesive and harder to handle.
How Micronization Works
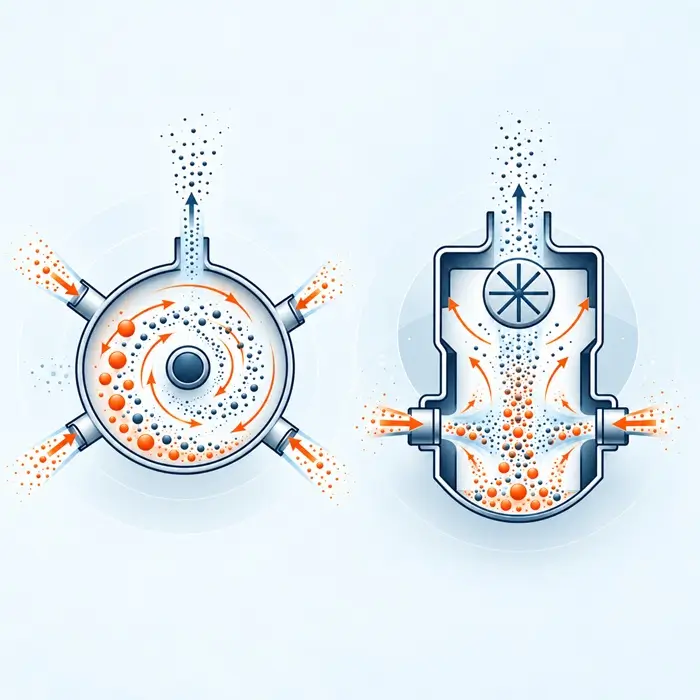
Jet milling is a common route to micronization. In jet mills, high-velocity gas jets accelerate particles so that they break mainly through collisions with each other. Many jet mills include an integrated classifier that returns oversize particles to the grinding zone, helping control the product’s upper size range.
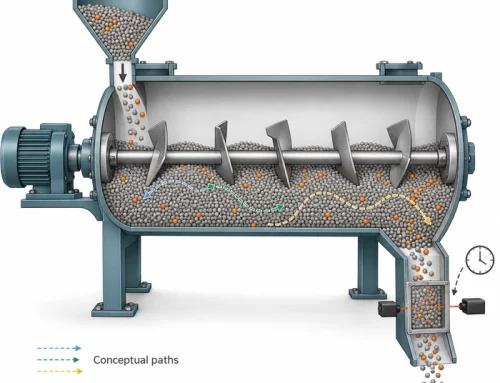
Other routes to fine particle sizes include ball mills, where a rotating drum filled with grinding media breaks material through impact and attrition, and stirred media mills, which apply more intensive stressing and are often used for wet fine grinding. The right choice depends on the target size, the material’s breakage behavior, heat sensitivity, and contamination limits.
Grinding and Shaping
Mills reduce particle size through a combination of stressing mechanisms: compression, impact, and shear or attrition. Which mechanism dominates depends on the mill type and operating conditions. It influences not only the final size but also particle shape, surface properties, and the amount of fines generated.
Laws of Comminution
It is difficult to predict the energy needed for size reduction precisely. Breakage behavior depends on factors including particle size, shape, internal structure, and mechanical properties. Only part of the supplied energy contributes to fracture and new surface formation; energy is also dissipated through friction, deformation, and heat.
Empirical relationships help estimate energy demand. They do not separately resolve every energy loss: their predictions depend on the test conditions and energy-measurement basis used to establish their constants.
Three classic laws remain useful for understanding these relationships. In the equations below, E is specific energy: energy per unit mass of material. For Kick’s and Rittinger’s equations, x1 and x2 represent characteristic feed and product sizes, using a consistent size definition and units. The fitted constants must match those choices.
Kick’s law
Kick’s law (1885) states that specific energy is proportional to the logarithm of the size-reduction ratio:
E = KK × ln(x1 / x2)
For equal masses of the same material, Kick’s law predicts the same specific energy for reduction from 10 to 5 mm as from 1 to 0.5 mm, provided the same fitted constant applies. Both steps have a size-reduction ratio of two.
Kick’s law is most often associated with coarse crushing, where the increase in specific surface area is relatively small.
Rittinger’s law
Rittinger’s law (1867) states that specific energy is proportional to the new surface area created. For particles of comparable shape and constant density, specific surface area scales inversely with particle size. The relationship can therefore be written as:
E = KR × (1/x2 − 1/x1)
Rittinger’s law is most often associated with fine grinding, where a large amount of new surface area is produced.
Both Kick’s and Rittinger’s constants are determined experimentally for a given material and set of milling conditions. The relationships can help compare size-reduction steps within a calibrated range, but their constants should not be transferred uncritically between materials or mills.
Bond’s law
In 1952, Bond proposed a method for estimating energy demand in crushing and grinding. Bond’s relationship expresses specific energy in terms of the difference between the inverse square roots of the product and feed sizes:
E = 10 × Wi × (1/√P80 − 1/√F80)
Here:
- E is specific energy in kWh per metric tonne.
- Wi is the applicable Bond work index, also expressed in kWh per metric tonne.
- P80 and F80 are the product and feed sizes, in micrometers, through which 80% of the respective material passes by mass.
Bond work indices are determined through specified laboratory tests. The appropriate index depends on the application: crushing, rod-mill, and ball-mill tests are distinct. The index characterizes resistance to comminution under the test conditions; it is not a universal constant independent of grinding size or test method.
Bond’s method is widely used in conventional mineral-processing grinding circuits. Applying it requires matching the test, equipment, and operating conditions, with correction factors where appropriate.
Worked Example
Consider a material with an illustrative Bond ball-mill work index of 12 kWh per metric tonne, ground from F80 = 2,000 µm to P80 = 75 µm:
E = 10 × 12 × (1/√75 − 1/√2,000)
E ≈ 11.2 kWh per metric tonne
This is a standard Bond energy estimate, not a measurement of the plant’s electricity consumption. Actual requirements depend on the equipment, circuit, and operating conditions. Comparisons must use a consistent energy boundary, such as the mill drive pinion for tumbling mills, and distinguish this from total plant demand.
For ball-mill products with a P80 below approximately 70 µm, the standard Bond method calls for a fineness correction; the 75 µm example sits just above that threshold.
The example illustrates conventional grinding rather than low-micrometer micronization. It should not be extrapolated directly to a jet-mill product of a few micrometers.
Comparing the Three Laws
| Law | Relationship | Common association | Main qualification |
|---|---|---|---|
| Kick’s | Specific energy varies with the logarithm of the reduction ratio. | Coarse crushing | Requires a constant calibrated for the material and conditions. |
| Bond’s | Specific energy varies with the difference in inverse square roots of feed and product sizes. | Conventional crushing and grinding | Requires the appropriate work-index test and applicable corrections. |
| Rittinger’s | Specific energy varies with the new surface area created. | Fine grinding | The size-based expression assumes comparable shape and constant density. |
These associations are approximate guides, not strict boundaries. A material’s behavior and the way a mill stresses its particles determine how well a relationship fits.
Choosing the Right Basis for Micronization
For low-micrometer micronization, none of these laws should be treated as a stand-alone equipment-sizing method. Agglomeration, classification, and changes in breakage behavior can affect the relationship between energy input and the measured product size.
Trials should establish whether the actual material reaches the required size distribution at an acceptable throughput, while meeting limits on temperature, contamination, and product quality. Energy measurements should also state what is included. For a jet-milling process, for example, compressed-gas generation is an important part of the energy demand.
Use the classic laws to understand trends and make estimates within an appropriate range. Use representative material trials to support equipment selection and performance expectations.
For guidance on choosing milling and classification equipment, see our Size Reduction & Classification guide.
Frequently Asked Questions
Technical Basis / Sources
- Global Mining Guidelines Group, Determining the Bond Efficiency of Industrial Grinding Circuits, 2021.
- Bond, F.C., “The Third Theory of Comminution,” Transactions of the AIME, Vol. 193, 1952.
- Rhodes, M.J. (ed.), Introduction to Particle Technology, 2nd ed., Wiley, 2008.
- Green, D.W. and Southard, M.Z. (eds.), Perry’s Chemical Engineers’ Handbook, 9th ed., McGraw-Hill Education, 2019, Section 21: Solids Processing and Particle Technology.
- Wills, B.A. and Finch, J.A., Wills’ Mineral Processing Technology, 8th ed., Butterworth-Heinemann, 2016.