Updated: November 18, 2026

Powders with the same chemical composition can behave differently in a feeder, dissolve at different rates, or form products with different mechanical properties. Their particle size distribution, shape, internal structure, and surface condition help explain why.
Particle engineering deliberately changes those attributes. Its value lies in connecting a measurable particle property to a practical outcome: more consistent dosing, faster reconstitution, controlled release, or more reliable processing. This is the opportunity behind the “golden goose” description, but the benefits depend on managing trade-offs.
What Is Particle Engineering?
Particle engineering involves designing or modifying particles to meet a performance requirement. It can take place while particles are formed, through processes such as crystallization or spray drying, or afterward through milling, classification, agglomeration, or coating.
The properties available for adjustment include:
- Particle size distribution: the proportions of fine and coarse particles, rather than a single average size.
- Shape: features such as roundness, elongation, and surface roughness.
- Internal structure: porosity, density, and whether a particle is solid, hollow, or an assembly of smaller particles.
- Surface properties: wettability, surface chemistry, and interactions with neighboring particles.
- Solid-state form: crystalline or amorphous structure, including different crystal forms where relevant.
These attributes interact. Milling may reduce size while changing shape and introducing defects. Spray drying can change particle structure and solid-state form as well as size. A useful specification therefore considers the properties that matter together, rather than optimizing one measurement in isolation.
Start With the Required Performance
“Improve the powder” is too broad to guide process development. A useful target describes what must happen and under which conditions.
For a feeder, the target might be a stable mass flow at the required throughput after storage. For an instant beverage, it might be rapid wetting and dispersion without persistent lumps. For a pharmaceutical product, it might be a defined dissolution profile, supported by appropriate product testing.
The next step is to identify which particle attributes plausibly control that outcome. Then select a process that changes those attributes without creating an unacceptable problem elsewhere.
| Required outcome | Particle attributes to investigate | Trade-off to check |
|---|---|---|
| Faster dissolution | Size distribution, accessible surface area, wettability, and solid-state form | Finer material may agglomerate or become harder to handle. |
| More consistent feeding | Fines content, shape, surface interactions, and moisture condition | Granules that flow well initially may break during transport. |
| Faster powder reconstitution | Agglomerate size, porosity, wettability, and strength | Agglomerates must survive handling but disperse during use. |
| Controlled release | Coating composition, thickness, continuity, and core properties | Coating defects or damage may change the release profile. |
| Reliable powder spreading | Size distribution, shape, surface condition, and density | A distribution that packs well may still spread unevenly. |
These are starting points for an investigation, not universal recipes.
Applications Across Industries
Pharmaceuticals
Particle size and solid-state form can influence dissolution, manufacturing behavior, and in some products bioavailability. However, a change in particle size does not by itself demonstrate improved absorption or therapeutic performance.
The distinction between dissolution rate and equilibrium solubility matters. Reducing particle size can increase the surface area available for dissolution. It should not automatically be described as increasing the amount that can dissolve at equilibrium. Changes in solid-state form can also affect solubility and stability, so they require separate consideration.
ICH Q6A identifies particle size and polymorphic form as attributes that may require control when they affect product performance. Their relevance must be established for the particular substance and dosage form. [1]
Food and Beverages
Particle engineering can change mouthfeel, handling, and reconstitution. Agglomeration, for example, can convert fine powder into larger, porous structures that wet and disperse more readily.
Wetting, dispersion, and dissolution are different steps. A powder may sink quickly but still leave undispersed lumps, or disperse readily while containing components that do not dissolve. The test should reflect how the customer prepares and uses the product.
Cosmetics and Functional Materials
In cosmetics, particle size, shape, and surface treatment influence spreading, texture, and appearance. In additive manufacturing, powder characteristics affect feeding and layer formation. In battery materials, particle structure and morphology contribute to processing and electrode behavior.
In each case, particle measurements help explain performance, but they do not replace application testing. A powder that meets a size specification may still fail because of surface condition, contamination, or handling history.
Why Smaller Particles Are Not Always Better
Micronization reduces particles into the micrometer range. Producing nanoscale material is a separate processing objective and should not be treated as an automatic extension of conventional micronization.
Size reduction can increase accessible surface area and accelerate dissolution. At the same time, surface forces become more important relative to particle weight, making fine powders more prone to cohesion and difficult flow.
Possible consequences include:
- Agglomeration that limits the surface area exposed during use.
- Less reliable discharge from hoppers or delivery through feeders.
- Greater sensitivity to moisture, depending on the material and environment.
- Increased dust generation and more demanding containment requirements.
Electrostatic charging can contribute to these problems, but it is not the only cause. Surface forces, moisture-related interactions, and mechanical interlocking may also matter.
The response should match the mechanism. Classification can remove an unwanted fine fraction. Agglomeration can improve handling. A suitable surface treatment may change particle interactions. Cryogenic milling can help process some heat-sensitive or ductile materials, while inert gas can limit oxidation or support a defined safety strategy; neither automatically solves poor flow.
Why Particle Size Distribution Matters
A single median size does not describe a powder adequately. Two powders can have the same median while containing very different amounts of fines and oversize particles.
A narrow distribution can be useful when a uniform response is required, but it does not guarantee good flow, stable suspensions, or consistent mixing. A broader or deliberately multimodal distribution may improve packing because smaller particles occupy spaces between larger ones. That same mixture may be more vulnerable to segregation during handling.
The appropriate distribution depends on the application. Specify relevant limits, such as excessive fines or an unacceptable coarse tail, and connect them to performance.
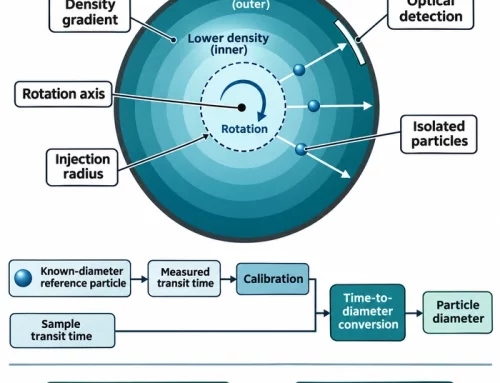
Measurement conditions also matter. A particle size result depends on sampling, dispersion, and the measurement principle. Laser diffraction, imaging, and dynamic light scattering do not report interchangeable quantities. Dynamic light scattering is primarily suited to particles dispersed in liquids within an appropriate measurement range; it is not a general substitute for characterizing dry bulk powders.
Choosing a Particle-Engineering Route
Several routes are available for particle formation and modification. The choice should follow the required properties and feed characteristics, rather than the name of the technology. [2, 3]
Milling and Classification
Milling breaks particles, while classification separates them according to their response in the classifier. Used together, they can control the product size distribution.
Trials should assess throughput, energy demand, temperature, contamination, and the amount of off-specification material, not just the final median size.
Agglomeration and Granulation
Agglomeration and granulation assemble smaller particles into larger structures. Depending on the process, liquid binders, mechanical agitation, or other bonding mechanisms provide cohesion.
Larger granules can reduce dust and improve handling. Porous agglomerates can also improve wetting and dispersion. These benefits depend on structure and strength: weak granules may generate fines during transport, while excessively strong granules may resist breakup during use.
Spray Drying
Spray drying converts a liquid feed into particles by atomizing it into droplets and evaporating the liquid. Feed composition, atomization, and drying conditions jointly influence particle size, morphology, residual moisture, and other properties. [3]
The process does not inherently guarantee a free-flowing powder. A formulation may produce sticky, cohesive, or fragile particles unless the formulation and operating conditions are developed together.
Coating and Encapsulation
Coating and encapsulation can protect an ingredient, modify surface interactions, mask taste, or control release.
Performance depends on the coating or matrix material, its distribution, and its integrity. A protective layer must remain effective after the handling and storage that the product will experience.
Verify the Improvement Under Real Conditions
Particle engineering is successful when the modified powder performs better in its intended application.
A practical development sequence is:
- Define the outcome. State the required performance, operating conditions, and acceptance criteria.
- Characterize the starting material. Use representative samples and record moisture condition, storage, and handling history.
- Select the intervention. Identify which properties the process should change and which must remain within limits.
- Measure both properties and performance. Confirm the particle changes and test their effect in the relevant operation.
- Challenge the result. Repeat the assessment after representative transport, storage, or processing.
For example, a granulated powder may feed consistently immediately after production but generate fines during conveying. Testing only the fresh granules would miss the condition that the feeder actually receives.
Similarly, faster dissolution after milling is useful only if the powder retains the necessary stability and can still be manufactured into a consistent product.
Where the Value Comes From
Particle engineering can reduce variability, improve product performance, and make processing more reliable. It can also add energy consumption, processing steps, yield losses, and quality-control requirements.
The commercial benefit therefore comes from the overall result: the performance gained relative to the cost and complexity introduced. There is no single ideal particle size, shape, or distribution for every powder.
Part 2 examines spray drying, fluid-bed agglomeration, and encapsulation. Part 3 covers micronization and the limits of the classic energy–size relationships used in comminution.
Frequently Asked Questions
Technical Basis / Sources
- FDA / ICH, Q6A: Specifications—Test Procedures and Acceptance Criteria for New Drug Substances and New Drug Products: Chemical Substances.
- Green, D.W. and Southard, M.Z. (eds.), Perry’s Chemical Engineers’ Handbook, 9th ed., McGraw-Hill Education, 2019.
- Masters, K., Spray Drying Handbook, 5th ed., Longman Scientific & Technical, 1991.
- Rhodes, M.J. (ed.), Introduction to Particle Technology, 2nd ed., Wiley, 2008.